
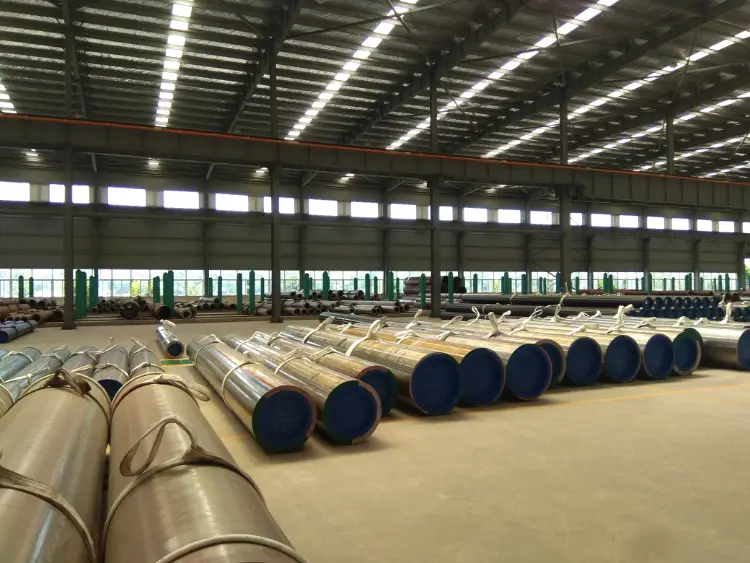
API 5L X80 PSL2 ERW Steel Pipe
API 5L X80 PSL2 ERW Steel Pipe - Material Data & Properties
Complete technical data for API 5L X80 PSL2 ERW steel pipe: chemical composition, mechanical and physical properties, international equivalents, and application guidance.
Electric resistance welding (ERW), heat treatment of weld seam as required
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
API 5L X80 PSL2 ERW Steel Pipe Introduction
API 5L X80 PSL2 ERW pipe is a high-strength, low-alloy (HSLA) steel pipe designed for long-distance oil and gas transmission. It is manufactured by electric resistance welding (ERW) from hot-rolled coils or plates. PSL2 imposes stricter requirements on chemical composition, notch toughness, and non-destructive inspection compared to PSL1.
The grade provides a minimum yield strength of 555 MPa (80 ksi), excellent weldability, and good low-temperature toughness, making it suitable for high-pressure, critical service pipelines in onshore and offshore environments.
API 5L X80 PSL2 ERW Steel Pipe Chemical Composition
Requirements according to API 5L (46th Ed.) for PSL2 pipe with thickness ≤ 25.0 mm. Carbon equivalent (CEIIW) is limited to ensure weldability. Microalloying elements Nb, V, Ti are used for grain refinement and precipitation strengthening. The sum of Nb + V + Ti shall not exceed 0.15%.
| Element | Specified Value (max, unless range) | Remarks |
|---|---|---|
| C | 0.22 | Heat analysis; product analysis tolerance applies |
| Si | 0.45 | For deoxidation |
| Mn | 1.85 | Maximum for PSL2; may be lower for thin walls |
| P | 0.025 | Strict control for toughness and HIC resistance |
| S | 0.015 | Low sulfur for improved formability and weldability |
| V | Report only | If intentionally added; part of Nb+V+Ti ≤ 0.15% |
| Nb | Report only | Grain refiner; part of Nb+V+Ti limit |
| Ti | Report only | Contains within Nb+V+Ti limitation |
| CEIIW | 0.43 (typically) | Carbon equivalent = C + Mn/6 + (Cr+Mo+V)/5 + (Ni+Cu)/15; limited for PSL2 |
API 5L X80 PSL2 ERW Steel Pipe Physical Properties
These values are not part of the API 5L specification but represent typical physical constants for low-carbon, low-alloy X80 pipe steel. They are valid for room temperature and atmospheric pressure, unless noted. Density and thermal expansion are sensitive to exact chemical composition.
| Property | Typical Value | Unit | Condition |
|---|---|---|---|
| Density (ρ) | 7850 | kg/m³ | Ambient temperature |
| Elastic Modulus (E) | 205 | GPa | Room temperature |
| Shear Modulus (G) | 80 | GPa | Calculated from E and ν |
| Poisson's Ratio (ν) | 0.3 | — | Elastic range |
| Thermal Expansion Coefficient (α) | 11.7 × 10⁻⁶ | K⁻¹ | 20–100°C |
| Thermal Conductivity (λ) | 50 | W/(m·K) | Room temperature |
| Specific Heat Capacity | 470 | J/(kg·K) | Room temperature |
| Electrical Resistivity (ρ_e) | 2.2 × 10⁻⁷ | Ω·m | Room temperature |
API 5L X80 PSL2 ERW Steel Pipe Mechanical Properties
Minimum and maximum values per API 5L PSL2 for X80 grade. Testing is performed on base metal transverse to the weld. Elongation is calculated from a 50 mm gauge length specimen according to the standard formula. Impact tests are required at a specified temperature (e.g., 0°C) for PSL2 qualification.
| Property | Required Value | Unit | Test Condition |
|---|---|---|---|
| Yield Strength (Rt0.5) | 555 – 705 | MPa | Transverse, base metal |
| Tensile Strength (Rm) | 625 – 825 | MPa | Transverse, base metal |
| Elongation (A) | ≥ 22 (typical) | % | 50 mm gauge, wall thickness ~12.5 mm |
| Bend Test | No cracks or openings | — | 180° bend with specified former, weld at point of max. bending |
| Charpy V-Notch Impact (base metal) | Avg. ≥ 27, Single ≥ 20 | J | Full-size specimen, 0°C or lower as agreed |
| Charpy V-Notch Impact (weld seam) | Avg. ≥ 27, Single ≥ 20 | J | Full-size specimen, same temperature as base |
| Hardness (HV10) | ≤ 270 (typically) | HV10 | Base metal and HAZ; may be specified for sour service |
API 5L X80 PSL2 ERW Steel Pipe Exact Equivalent Standards and Substitutable Grades
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| International | ISO 3183 | L555Q or L555M | Q – quenched and tempered; M – thermomechanical rolled |
| Europe | EN 10208-2 | L555MB | For onshore steel pipes; M – thermomechanical treatment |
| China | GB/T 9711 | L555Q / L555M | Equivalent to PSL2 requirements |
| Canada | CSA Z245.1 | Grade 550 Category II | Close chemical and mechanical match |
| Russia | GOST R ISO 3183 | K60 (strength class) | Similar strength level; verify PSL2 toughness requirements |
API 5L X80 PSL2 ERW Steel Pipe Application Introduction
API 5L X80 PSL2 ERW pipe is primarily employed in high-pressure, long-distance transmission pipelines for natural gas and crude oil. Its high strength-to-weight ratio allows thinner walls for the same pressure rating, reducing material and transportation costs. The ERW manufacturing process offers tight dimensional tolerances and is well suited for medium-diameter (up to 24 inch NPS) onshore and some offshore applications.
Product Applications: Cross-country transmission pipelines, Flowlines and gathering lines for natural gas, Subsea tie-backs and risers (when coated/insulated), Station piping within compressor/pumping facilities
Processed into products: Line pipe spools and straight run pipe, Induction bends (hot-formed from X80 pipe), Cold-formed elbows, tees, reducers, Welded flanges and connectors, Pressure-containing parts for pig launchers/receivers
Application industries: Oil and gas exploration & production, Pipeline transmission (onshore & offshore), Petrochemical and refining, Natural gas distribution and gathering, Water transmission (when strength is needed)
API 5L X80 PSL2 ERW Steel Pipe Near-equivalent and Similar Alternative Materials
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| USA | API 5L | X80 PSL1 | Same strength, relaxed chemistry and toughness – not for critical service |
| USA | API 5L | X70 PSL2 | Slightly lower strength (485 MPa min yield); heavier wall may be required |
| International | ISO 3183 | L555Q (PSL1) | When PSL2 toughness is not mandatory |
| Europe | EN 10208-2 | L555MA | Alloy design with different delivery condition |
| China | GB/T 9711 | L555 (non-PSL restrained) | Check PSL2 requirements if toughness is critical |
Notes:
ERW pipe manufactured to API 5L PSL2 requires post-weld heat treatment of the seam (normalizing or stress-relieving) to achieve uniform hardness and toughness across the weld, base metal, and heat-affected zone. Additional supplementary requirements (e.g., HIC/SSC testing for sour service, fracture toughness CTOD testing) may be specified by the purchaser. Welding consumables and procedures for site girth welding must be qualified for the X80 grade to avoid hydrogen-induced cracking. Magnetic particle or ultrasonic inspection of the weld seam is mandatory for PSL2.
- Share



