
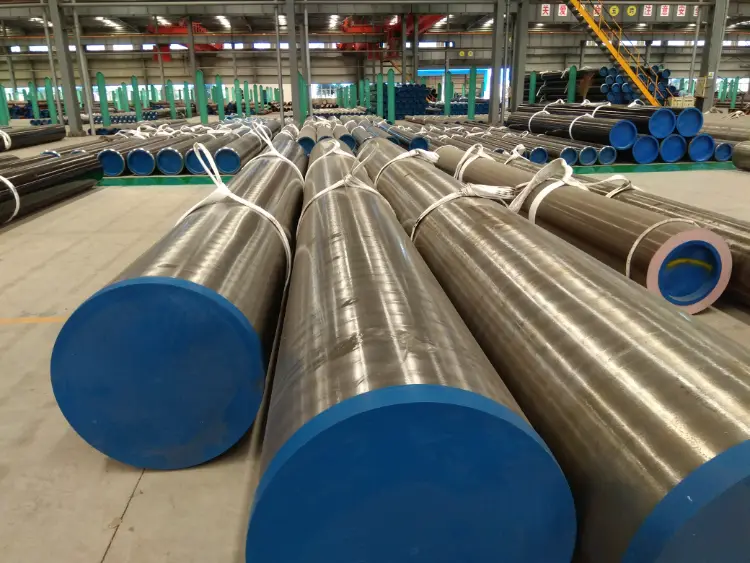
API 5L PSL2 Grade B SSAW Pipe
API 5L Grade B SSAW Pipe: Chemical and Mechanical Properties, Equivalents | Material Data
Explore detailed material properties of API 5L PSL2 Grade B for spiral submerged arc welded pipe, including chemistry, mechanical, thermal characteristics, and global equivalents.
Spiral forming and submerged arc welding (SAW) with high-speed welding and both internal and external welding passes
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
API 5L PSL2 Grade B SSAW Pipe Introduction
API 5L Grade B is a widely used carbon-manganese steel for line pipe, specified under the American Petroleum Institute (API) Standard 5L, Product Specification Level 2 (PSL2). It is mainly supplied as spiral submerged arc welded (SSAW) pipe for conveying oil, gas, and water. PSL2 imposes stricter chemical composition, mechanical properties, and mandatory non-destructive testing compared to PSL1. The steel exhibits a minimum yield strength of 245 MPa, good ductility, and excellent field weldability. Typical delivery condition for SSAW pipe is as-welded, but normalizing may be applied to achieve specified properties.
- Minimum yield strength 245 MPa (35.5 ksi)
- Controlled carbon equivalent CEV ≤ 0.43% for good weldability
- Excellent low-temperature toughness with Charpy requirements (typically 27 J at 0 °C)
- Recognized internationally as L245 in ISO 3183 and GB/T 9711
API 5L PSL2 Grade B SSAW Pipe Chemical Composition
The chemical composition of API 5L PSL2 Grade B strictly follows the melt analysis requirements of API 5L 46th Edition. The carbon equivalent (CEV) is limited to ensure good weldability. Residual elements are controlled though not individually mandated for Grade B; when present, they contribute to the CEV formula.
| 化学元素 | 标准值 | 备注说明 |
|---|---|---|
| C | ≤ 0.22 | Melt analysis, maximum |
| Mn | ≤ 1.20 | Melt analysis, maximum |
| P | ≤ 0.025 | Maximum |
| S | ≤ 0.015 | Maximum |
| Si | Not specified | Typically 0.15–0.35 for deoxidation |
| CEV | ≤ 0.43 | CEV = C + Mn/6 + (Cr+Mo+V)/5 + (Ni+Cu)/15, based on product analysis |
| Cu, Ni, Cr, Mo | Not individually limited | Subject to CEV calculation; trace amounts typical |
API 5L PSL2 Grade B SSAW Pipe Thermal, Electrical and Physical Properties
The following physical properties are typical for hot-rolled carbon steel and are not specified in API 5L. They serve as general reference data for engineering calculations at ambient temperature unless otherwise noted.
| 性能项目 | 标准要求值 | 单位 | 测试条件 |
|---|---|---|---|
| Density (ρ) | 7850 | kg/m³ | Approximate at 20 °C |
| Modulus of elasticity (E) | 210 | GPa | At 20 °C, static |
| Shear modulus (G) | 81 | GPa | At 20 °C |
| Poisson's ratio (ν) | 0.3 | — | Elastic range |
| Coefficient of thermal expansion (α) | 12.0 | 10⁻⁶/K | 20–100 °C |
| Thermal conductivity (λ) | 50 | W/(m·K) | At 20 °C |
| Specific heat capacity (cp) | 460 | J/(kg·K) | At 20 °C |
| Electrical resistivity (ρe) | 0.20 | µΩ·m | At 20 °C |
API 5L PSL2 Grade B SSAW Pipe Mechanical Properties
Tensile and impact properties are determined on transverse test pieces taken from the pipe body in accordance with API 5L. Values below represent the minimum and maximum requirements for PSL2 Grade B. Notch toughness depends on the service temperature and supplemental requirements; the 27 J average at 0 °C is a common specification.
| 性能项目 | 标准要求值 | 单位 | 测试条件 |
|---|---|---|---|
| Yield Strength (Rt0.5) min | 245 | MPa | Transverse strip specimen, pipe body |
| Yield Strength (Rt0.5) max | 450 | MPa | Transverse strip specimen, pipe body |
| Tensile Strength (Rm) min | 415 | MPa | Transverse strip specimen, pipe body |
| Tensile Strength (Rm) max | 655 | MPa | Transverse strip specimen, pipe body |
| Elongation after fracture (A) min | 22 | % | Gauge length 50 mm, transverse strip, wall ≤ 25.4 mm |
| Rt0.5/Rm ratio | ≤ 0.93 | — | Transverse |
| Charpy V-notch impact energy (KV) average | 27 | J | Full-size 10×10 mm, transverse, at 0 °C (typical) |
| Charpy V-notch impact energy (KV) single minimum | 20 | J | Full-size 10×10 mm, transverse, at 0 °C (typical) |
API 5L PSL2 Grade B SSAW Pipe Exact Equivalent Standards and Alternative Grades
| 国家/地区 | 执行标准 | 牌号 | 备注说明 |
|---|---|---|---|
| International | ISO 3183 | L245 PSL2 | Identical technical requirements |
| China | GB/T 9711 | L245 PSL2 | Aligned with API 5L |
| European Union | EN 10208-2 | L245NB | Normalizing rolled, equivalent to PSL2 when impact-tested |
| Russia/CIS | GOST R 52079 | K52 (17G1S) | Similar yield class, often used as substitute |
API 5L PSL2 Grade B SSAW Pipe Application Introduction
API 5L Grade B SSAW pipe is the backbone of long-distance oil and gas pipelines. It is also used in water transmission and structural applications where a balanced combination of strength, ductility, and field weldability is required. The pipe is typically buried or submerged, and its spiral weld is inspected via automatic ultrasonic or radiographic testing per PSL2 requirements.
Product Applications: Cross-country oil and gas pipelines, High-pressure water mains, Piling pipes for foundation support, Casing and tubing strings in wells (limited use)
Processed into products: Pipeline girth welds and fittings (elbows, tees, reducers), Flanges manufactured from matching pipe material, Vessels and storage tanks made from welded pipe sections, Structural columns and braces
Application industries: Oil & Gas (upstream and midstream), Water and wastewater management, Construction and civil engineering, Mining (slurry transport)
API 5L PSL2 Grade B SSAW Pipe Similar/Comparable Materials for Substitution
| 国家/地区 | 执行标准 | 牌号 | 备注说明 |
|---|---|---|---|
| United States | ASTM A53/A53M | Grade B Type E/W | Seamless/welded pipe, similar strength but less stringent than PSL2 |
| United States | ASTM A106/A106M | Grade B | Seamless carbon steel for high-temperature service; not identical to line pipe |
| Japan | JIS G3454 | STPG370 | Pressure piping steel, comparable tensile range |
| Europe | EN 10217-1 | P235TR1 | Welded steel tubes with slightly lower strength |
Notes:
Additional remarks:
- SSAW pipe is produced from hot-rolled coil; the spiral weld seam is subject to 100 % non-destructive test (UT or X-ray) per PSL2.
- For sour service (H₂S), supplementary requirements per API 5L Annex H must be specified, which may require lower hardness and special welding consumables.
- Material certificates must comply with API 5L, including chemical analysis, tensile test, Charpy test (if ordered), and hydrostatic test results.
- Share



