
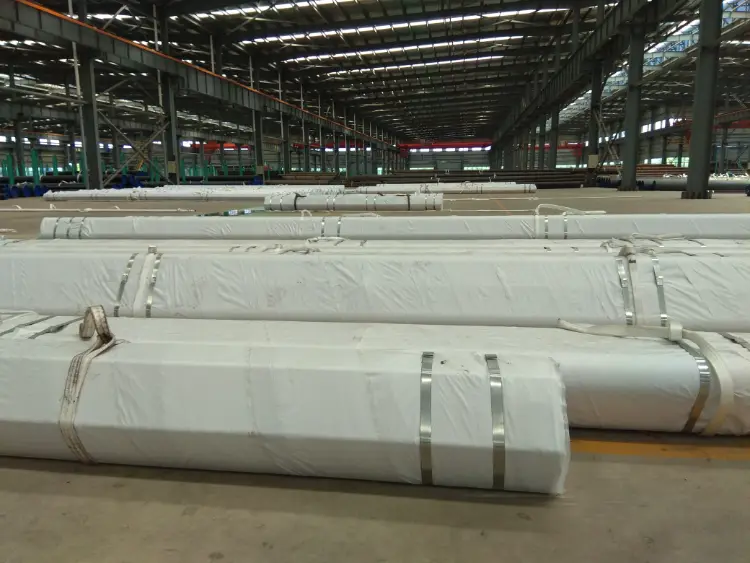
API 5L X42 PSL2 SSAW Pipe
API 5L X42 PSL2 SSAW Pipe: Comprehensive Material Properties and Equivalents
Explore the complete material data for API 5L X42 PSL2 SSAW (Spiral Submerged Arc Welded) pipe. Includes official chemical composition, mechanical properties, thermal and electrical characteristics, and global equivalent grades for seamless substitution.
Hot‑rolled steel strip/plate, forming, submerged arc welding, and optional post‑weld heat treatment. Suitable for bending, cutting, welding, and coating.
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
API 5L X42 PSL2 SSAW Pipe Introduction
API 5L X42 PSL2 is a high-strength carbon steel line pipe grade produced according to the American Petroleum Institute specification API 5L, with Product Specification Level 2 (PSL2) requirements. The SSAW (Spiral Submerged Arc Welded) manufacturing process ensures excellent dimensional accuracy and mechanical integrity for medium‑diameter pipelines.
Key features include:
- Yield strength: minimum 290 MPa (42 ksi), with an upper limit of 496 MPa (72 ksi) to guarantee controlled ductility.
- PSL2 toughness: mandatory Charpy V‑notch impact testing at low temperatures, ensuring reliable performance in harsh environments.
- Weldability: controlled carbon equivalent (CE) for excellent field weldability.
- Corrosion resistance: typical carbon steel behavior, suitable for non‑sour service unless supplementary requirements (e.g., HIC/SSC testing) are specified.
This grade is extensively used for oil and gas transmission pipelines, water distribution networks, and structural piling applications.
API 5L X42 PSL2 SSAW Pipe Chemical Composition
The chemical requirements for API 5L X42 PSL2 are based on heat analysis, with slightly relaxed product analysis limits. The table lists the maximum permissible values for elements that directly influence strength, toughness, and weldability. A maximum carbon equivalent (CEIIW) of 0.43% is mandatory for PSL2 to ensure good field weldability. Residual elements like Cr, Ni, Mo, and Cu are not specified but, if present, shall be reported.
| Element | Standard Value (Max, %) | Remarks |
|---|---|---|
| Carbon (C) | 0.24 | For heat analysis; 0.26 % for product analysis |
| Manganese (Mn) | 1.30 | Maximum for heat analysis |
| Phosphorus (P) | 0.025 | PSL2 strict limit for improved toughness |
| Sulfur (S) | 0.015 | PSL2 low sulfur requirement |
| Silicon (Si) | 0.40 | Typical for deoxidation and strength |
| Vanadium (V) | 0.05 | Optional microalloying element |
| Niobium (Nb) | 0.05 | Optional microalloying element |
| Titanium (Ti) | 0.04 | Optional grain refiner |
| Carbon Equivalent (CE) | 0.43 | Calculated per IIW formula: C + Mn/6 + (Cr+Mo+V)/5 + (Ni+Cu)/15 |
API 5L X42 PSL2 SSAW Pipe Thermal and Electrical Physical Properties
The following physical constants are typical for carbon‑manganese pipeline steel at room temperature and are not specified in API 5L. They serve as design reference values. Slight variations may occur depending on manufacturing process and composition.
| Property | Typical Value | Unit | Test Condition / Remarks |
|---|---|---|---|
| Density (ρ) | 7.85 | g/cm³ | 20 °C |
| Elastic Modulus (E) | 205 – 210 | GPa | Room temperature, tensile test |
| Shear Modulus (G) | ~80 | GPa | Calculated from E and ν |
| Poisson's Ratio (ν) | 0.29 – 0.30 | — | Within elastic range |
| Thermal Expansion Coefficient (α) | 11.7 | 10⁻⁶/K | 20–100 °C |
| Thermal Conductivity (λ) | 50 | W/(m·K) | At 20 °C; varies with temperature |
| Specific Heat Capacity | 460 – 500 | J/(kg·K) | Room temperature |
| Electrical Resistivity (ρₑ) | 0.15 – 0.18 | μΩ·m | At 20 °C |
API 5L X42 PSL2 SSAW Pipe Mechanical Properties
Mechanical properties are determined in accordance with API 5L test methods. For PSL2, the yield strength has both a minimum and a maximum to ensure controlled plastic deformation capacity. Charpy impact values are mandatory for PSL2; the table shows typical requirements for transverse specimens. Elongation is calculated using the API 5L formula, but a representative minimum value for common wall thicknesses is given.
| Property | Required Value | Unit | Test Condition / Remarks |
|---|---|---|---|
| Yield Strength (ReH) | 290 – 496 | MPa | 0.2 % offset; limits for PSL2; 42–72 ksi |
| Tensile Strength (Rm) | ≥ 414 | MPa | Minimum; 60 ksi. No upper limit specified |
| Elongation (A) | ≥ 23 (typical) | % | In 2 in. (50 mm); depends on specimen area. API 5L formula gives minimum |
| Transverse Charpy V‑Notch (KV) | ≥ 27 (avg) / 22 (single) | J | Full‑size specimen at 0 °C or as agreed; 20/16 ft·lb |
| Longitudinal Charpy V‑Notch (KV) | ≥ 41 (avg) / 30 (single) | J | Full‑size specimen at 0 °C or as agreed; 30/22 ft·lb |
API 5L X42 PSL2 SSAW Pipe Fully Equivalent Material Standards and Substitutable Grades
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| International | ISO 3183 | L290 (PSL 2) | Identical technical requirements; L290 matches X42 yield strength |
| Europe | EN 10208‑2 | L290MB | Welded line pipe for combustible fluids; MB suffix indicates PSL2‑like quality |
| Canada | CSA Z245.1 | Grade 290 Cat II | Category II corresponds to PSL2 with toughness requirements |
| China | GB/T 9711 | L290 | Chinese line pipe standard, equivalent to ISO 3183 L290 |
API 5L X42 PSL2 SSAW Pipe Application Introduction
API 5L X42 PSL2 SSAW pipe is a versatile material for onshore and offshore hydrocarbon transportation, as well as for water and structural applications. Its balanced strength and excellent weldability make it a preferred choice for medium‑pressure pipelines. Typical applications are listed below.
Product Applications: Crude oil and natural gas transmission pipelines, Product and gathering lines, Water mains and distribution networks, Structural pipe piles and casings, Penstocks and pressure tunnels
Processed into products: Line pipe joints (straight and spiral welded), Induction bends, Weldolets and branch connections, Flanges and backing rings, Pipeline fittings (tees, reducers, caps)
Application industries: Oil & Gas (upstream and midstream), Petrochemical & Refining, Water & Wastewater Treatment, Civil Engineering & Construction, Mining & Slurry Transport
API 5L X42 PSL2 SSAW Pipe Similar or Alternative Line Pipe Grades
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| USA / International | API 5L | X46 | Higher strength (min YS 320 MPa); same PSL2 options, often used for higher pressure lines |
| USA / International | API 5L | X52 | Further increase in strength (min YS 360 MPa); may require stricter welding procedures |
| International | ISO 3183 | L320 / L360 | Correspond to X46 and X52 respectively; suitable when higher strength is needed |
| Europe | EN 10208‑2 | L290NB | Non‑alloy steel with lower toughness (PSL1‑like); may be used in less critical service |
Notes:
This data is compiled from API 5L 46th edition and allied international standards. PSL2 requirements encompass mandatory Charpy testing, non‑destructive examination (NDE) for seam weld, and traceability. SSAW pipe is produced by helically forming hot‑rolled coil and welding with submerged arc process. Additional supplementary requirements (like HIC/SSC resistance for sour service) may be agreed upon.
- Share



