
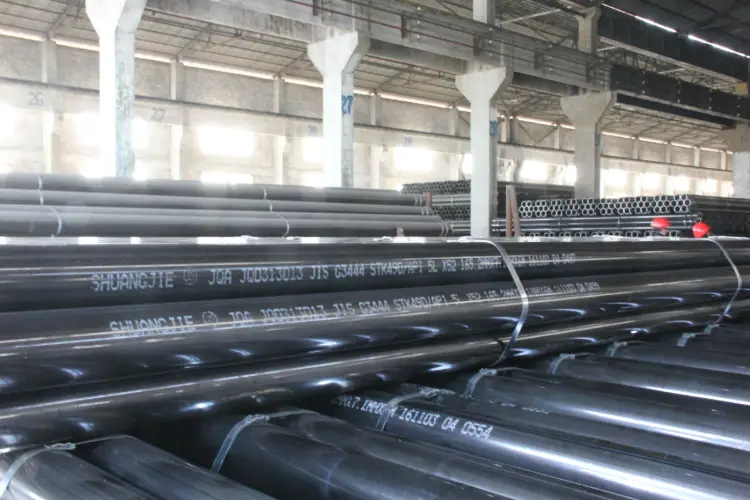
API 5L PSL2 X52 ERW Pipe
API 5L PSL2 X52 ERW Pipe: High Strength Line Pipe for Oil & Gas Transmission
Comprehensive material data for API 5L PSL2 grade X52 electric resistance welded pipe, covering chemical composition, mechanical properties, thermophysical and electrical properties, international equivalents, and typical applications.
Electric resistance welding (ERW), submerged arc welding (SAW), seamless; available processing includes cutting, beveling, bending, and coating
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
API 5L PSL2 X52 ERW Pipe Introduction
API 5L X52 PSL2 ERW pipe is a high-strength line pipe produced by electric resistance welding (ERW) conforming to the stringent product specification level 2 (PSL2) of API Spec 5L. It is primarily intended for conveying oil, gas, and water in the petroleum and natural gas industries. This grade offers a minimum yield strength of 52 ksi (359 MPa) and enhanced toughness requirements, ensuring reliable performance in demanding pipeline applications. PSL2 imposes tighter chemical composition limits, mandatory Charpy impact testing, and non-destructive inspection, making it suitable for sour service and low-temperature environments. Typical delivery condition is as-rolled, normalized, or thermomechanically processed, providing a fine-grained microstructure for improved weldability and ductility.
API 5L PSL2 X52 ERW Pipe Chemical Composition
Chemical requirements for API 5L X52 PSL2 pipe as per API 5L 46th edition. Maximum limits are given unless a range is specified. Residual elements are controlled to ensure weldability and toughness. Carbon equivalent (CEIIW) limits apply depending on wall thickness and service conditions.
| Element | Standard Value | Remarks |
|---|---|---|
| C | ≤0.28 | max |
| Mn | ≤1.40 | max, for wall thickness ≤25 mm |
| P | ≤0.025 | max |
| S | ≤0.015 | max |
| V | ≤0.06 | max; when V+Nb+Ti ≤0.15% |
| Nb | ≤0.06 | max; when V+Nb+Ti ≤0.15% |
| Ti | ≤0.06 | max; when V+Nb+Ti ≤0.15% |
| Si | ≤0.45 | max |
| Cu | ≤0.50 | max |
| Ni | ≤0.50 | max |
| Cr | ≤0.50 | max |
| Mo | ≤0.50 | max |
| Al | ≤0.060 | max, total aluminum |
| N | ≤0.012 | max |
| B | ≤0.0005 | max, if not intentionally added |
| CEIIW | ≤0.43 | max, for wall thickness ≤25 mm; other limits apply based on grade and thickness |
API 5L PSL2 X52 ERW Pipe Thermophysical and Electrical Properties
Thermophysical and electrical properties are typical for API 5L X52 carbon‑manganese steel at room temperature. These values are not specified in API 5L but are representative for line pipe steel. Variations may occur depending on exact composition and heat treatment.
| Property | Typical Value | Unit | Test Condition |
|---|---|---|---|
| Density (ρ) | 7.85 | g/cm³ | 20°C |
| Elastic Modulus (E) | 205 | GPa | ambient temperature |
| Shear Modulus (G) | 79 | GPa | calculated from E, ν |
| Poisson's Ratio (ν) | 0.30 | elastic, room temperature | |
| Thermal Expansion Coefficient (α) | 11.7 | µm/m·K | 20–100°C |
| Thermal Conductivity (λ) | 50 | W/m·K | 20°C |
| Specific Heat Capacity (cp) | 480 | J/kg·K | 20°C |
| Electrical Resistivity (ρe) | 0.15 | µΩ·m | 20°C |
API 5L PSL2 X52 ERW Pipe Mechanical Properties
Mechanical properties for API 5L X52 PSL2 pipe according to API 5L specification. The values apply to the pipe body except where noted. Charpy impact test is mandatory for PSL2; typical test temperature is 0°C (32°F) with a minimum average absorbed energy of 27 J for full-size transverse specimens. Hardness values are maximums for the parent metal.
| Property | Standard Requirement | Unit | Test Condition |
|---|---|---|---|
| Yield Strength (ReH) | 359–530 | MPa | Transverse strip, 0.5% total extension under load |
| Tensile Strength (Rm) | 455–760 | MPa | Transverse strip |
| Elongation (A) | ≥22 | % | 50 mm gauge length (2 in), proportional to specimen area; exact requirement depends on sample UTS |
| Yield to Tensile Ratio | ≤0.93 | As required by PSL2 | |
| Charpy Impact Energy (KV) | ≥27 (average) / ≥21 (single) | J | Full-size (10×10 mm) transverse specimen, 0°C (32°F) |
| Hardness | ≤250 HV10 | HV | Parent metal, all locations; for weld metal and HAZ: ≤275 HV10 |
API 5L PSL2 X52 ERW Pipe Fully Equivalent Material Standards and Replaceable Grades
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| International | ISO 3183 | L360 | PSL2, welded or seamless |
| Europe | EN 10208-2 | L360NB/L360MB | Requirements similar to API X52 PSL2; NB: normalized, MB: thermomechanical |
| China | GB/T 9711 | L360 | Line pipe for petroleum and natural gas industries |
| USA | API 5L | X52 PSL2 | Original specification |
| Russia | GOST 20295 | К52 | Strength class K52; grade analogous |
API 5L PSL2 X52 ERW Pipe Application Introduction
API 5L X52 PSL2 ERW pipe is extensively used in the oil and gas industry for long‑distance transmission of crude oil, natural gas, and refined products. Its high strength-to-weight ratio, good weldability, and adequate low‑temperature toughness make it suitable for both onshore and offshore applications. The ERW manufacturing process ensures consistent dimensions and surface quality, facilitating coating and field welding.
Product Applications: Mainline oil and gas pipelines, Flowlines and gathering lines, Water injection and disposal lines, Structural columns and bollards, Piling pipe for foundations, Process piping in refineries
Processed into products: Straight pipe segments and bends, Pipe fittings (elbows, tees, reducers), Flanges (weld neck, slip-on), Valve bodies and adapters, Riser sections for offshore platforms, Tubular joints and connectors
Application industries: Oil and gas exploration and production, Petrochemical processing, Water and wastewater transmission, Civil engineering and construction (structural pipe), Marine and offshore engineering, Power generation
API 5L PSL2 X52 ERW Pipe Similar / Alternative Material Suggestions
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| USA | API 5L | X46 PSL2 | Lower strength, higher toughness; may be used where design stress is lower |
| USA | API 5L | X56 PSL2 | Slightly higher strength; suitable for higher pressure pipelines |
| USA | ASTM A53 | Grade B | Seamless/welded pipe for mechanical and pressure applications, lower yield (240 MPa) |
| USA | ASTM A106 | Grade B | Seamless carbon steel pipe for high-temperature service, comparable tensile but lower yield |
| Europe | EN 10217-3 | P355N | Welded steel tubes for pressure purposes, normalized, similar strength range |
Notes:
For sour service applications (H2S-containing environments), supplementary requirements such as HIC/SWC testing per NACE TM0284 and hardness limits for weld zones may be mandated by the purchase specification. ERW pipe should be subjected to post‑weld heat treatment (PWHT) if required by the service conditions. Coating with fusion‑bonded epoxy (FBE) or three‑layer polyethylene (3LPE) is typical for buried pipelines. Charpy impact test temperature can be lowered to –45°C for Arctic service upon agreement. Dimensional tolerances are in accordance with API 5L; wall thickness tolerance is –12.5%/+15% for ERW pipe unless tighter restrictions are specified.
- Share



