
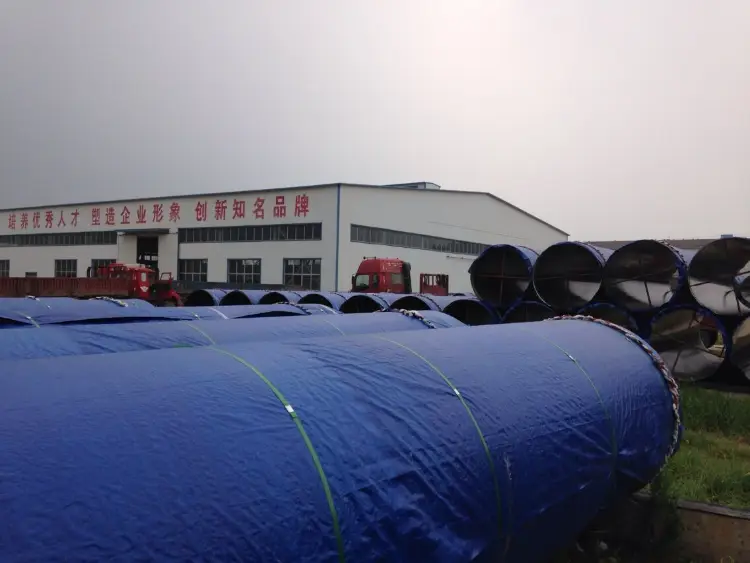
EN10219 S355K2H LSAW Steel Pipe
EN10219 S355K2H LSAW Steel Pipe - High-Strength Cold-Formed Hollow Section for Demanding Structural Applications
Comprehensive technical data sheet for S355K2H cold-formed welded steel hollow section according to EN10219. Includes chemical composition, mechanical properties, physical characteristics, and international equivalents. Used in construction, machinery, offshore, and heavy engineering projects requiring low-temperature toughness.
Cold forming, welding (submerged arc), normalising (if required), straightening, cutting, machining, galvanizing
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
EN10219 S355K2H LSAW Steel Pipe Introduction
S355K2H is a cold-formed welded structural steel hollow section (LSAW pipe) conforming to EN 10219-1. It is a fine-grain structural steel with a minimum yield strength of 355 MPa and guaranteed Charpy impact energy of 27 J at -20 °C (designated K2). The 'H' indicates a hollow profile. Produced by longitudinal submerged arc welding (LSAW), it combines high strength with excellent weldability and cold forming characteristics.
- Available in square, rectangular, and circular hollow sections.
- Ideal for dynamically loaded structures, bridges, cranes, and offshore platforms where low-temperature toughness is critical.
- Delivered in the as-welded or normalised condition depending on the manufacturing process and agreement.
EN10219 S355K2H LSAW Steel Pipe Chemical Composition
Elements according to EN 10219-1:2006, Table 2 for fine-grain steel grade S355K2H. Values apply to the heat (ladle) analysis. The steel is fully killed and contains fine-grain forming elements such as aluminium, niobium, vanadium, or titanium. No intentional addition of boron is allowed unless for specific purpose. Note: S355K2H may have microalloying elements not individually specified but controlled to meet mechanical properties.
| Element | Standard Value (max, unless specified) | Remarks |
|---|---|---|
| Carbon (C) | ≤ 0.20 | Typical values may be lower for improved weldability |
| Silicon (Si) | ≤ 0.55 | Deoxidation element |
| Manganese (Mn) | ≤ 1.60 | Contributes to strength and toughness |
| Phosphorus (P) | ≤ 0.035 | Impurity, lower is better for toughness |
| Sulfur (S) | ≤ 0.035 | Impurity, kept low for weldability |
| Nitrogen (N) | ≤ 0.012 | For fine-grain steels; higher N may require additional fixing elements |
| Aluminium (Al) | ≥ 0.020 (total) | Required for fine-grain practice; metallic Al or Al+Nb/V/Ti |
| Niobium (Nb) | ≤ 0.05 | Optional microalloy (if present) |
| Vanadium (V) | ≤ 0.12 | Optional microalloy (if present) |
| Titanium (Ti) | ≤ 0.05 | Optional microalloy (if present) |
| Molybdenum (Mo) | ≤ 0.10 | Residual or trace element |
| Nickel (Ni) | ≤ 0.30 | Residual |
| Chromium (Cr) | ≤ 0.30 | Residual |
| Copper (Cu) | ≤ 0.35 | Residual; higher values only by agreement |
EN10219 S355K2H LSAW Steel Pipe Thermal and Electrical Physical Properties
Typical physical properties for S355K2H steel at room temperature and elevated temperatures. These values are representative for structural carbon-manganese steels and may vary slightly depending on exact composition and processing. Density is standard for steel; elastic moduli are nominal for design. Thermal expansion coefficient and thermal conductivity follow EN 1993-1-2 for structural fire design.
| Property | Typical Value | Unit | Reference Condition |
|---|---|---|---|
| Density (ρ) | 7850 | kg/m³ | At 20 °C |
| Elastic modulus (E) | 210 | GPa | At 20 °C |
| Shear modulus (G) | 81 | GPa | At 20 °C |
| Poisson's ratio (ν) | 0.3 | – | Within elastic range |
| Coefficient of thermal expansion (α) | 12 × 10⁻⁶ | K⁻¹ | Between 20 °C and 100 °C |
| Thermal conductivity (λ) | 50 | W/(m·K) | At 20 °C |
| Specific heat capacity (Cp) | 480 | J/(kg·K) | At 20 °C |
| Electrical resistivity (ρ_e) | 0.22 × 10⁻⁶ | Ω·m | At 20 °C, typical for low-alloy steel |
EN10219 S355K2H LSAW Steel Pipe Mechanical Properties
Requirements according to EN 10219-1, for thickness ≤ 16 mm. Values are valid for the flat faces of the hollow section, tested in the longitudinal direction. Transverse properties may be slightly lower.
- ReH (Upper Yield Strength): Minimum 355 MPa.
- Rm (Tensile Strength): 470 – 630 MPa.
- A (Elongation after fracture): Minimum 20% on a gauge length of 5.65√S₀.
- Charpy V-notch impact energy (KV): 27 J minimum at -20 °C (K2 quality).
- Bend test: Full section flattening or bend test with mandrel diameter dependent on wall thickness, no cracks permitted.
| Property | Standard Requirement | Unit | Test Condition |
|---|---|---|---|
| Upper yield strength (ReH) | ≥ 355 | MPa | Wall thickness t ≤ 16 mm, longitudinal specimen |
| Tensile strength (Rm) | 470 – 630 | MPa | t ≤ 16 mm |
| Elongation after fracture (A) | ≥ 20 | % | t ≤ 16 mm, gauge length 5.65√S₀, longitudinal |
| Charpy impact energy (KV) | ≥ 27 | J | At -20 °C, longitudinal specimen, full-size V-notch |
| Bend test (flattening) | No cracks or flaws | – | Flat test for circular tubes; bend radius depends on diameter/wall thickness |
| Welded joint strength | ≥ tensile strength of base metal | MPa | Transverse weld tensile test, fracture outside weld |
EN10219 S355K2H LSAW Steel Pipe Completely Equivalent Material Standards and Replaceable Grades
| Country / Region | Standard | Grade | Remarks |
|---|---|---|---|
| European Union | EN 10210-1 (hot finished) | S355K2H | Hot-finished counterpart with identical mechanical/chemical requirements but different production route |
| United Kingdom | BS EN 10219-1 | S355K2H | Direct adoption of EN standard |
| Japan | JIS G 3475 / JIS G 3466 | STKR490 / STKN490B | Similar strength level with guaranteed low-temperature toughness; specific K2 impact matches STKN490B |
| China | GB/T 1591 / GB/T 6728 | Q355D (for hollow sections) | Q355D provides -20 °C toughness, equivalent to S355K2 requirement |
| International | ISO 630-2 | S355K2 | Base standard for structural steels; product form equivalence for hollow sections not covered |
EN10219 S355K2H LSAW Steel Pipe Application Introduction
S355K2H LSAW pipes and hollow sections are selected for structures exposed to dynamic loading, low temperatures, and demanding durability requirements. The combination of high yield strength, good weldability, and guaranteed -20 °C impact toughness makes them suitable for a wide range of indoor and outdoor projects. Common uses span building frames, heavy equipment, and marine infrastructure.
Product Applications: Structural columns, beams, and truss members, Crane jibs, booms, and lattice structures, Offshore structural components (legs, braces), High-strength scaffolding and formwork, Container and trailer frames, Wind turbine towers (sub-sections), Railway bridges and pedestrian overpasses
Processed into products: Welded nodes and gusset plates for trusses, Pin-jointed connectors for modular structures, Cylindrical spacers and bearing sleeves, Foundation piles and casings, Bent or rolled curved members (if cold formed within limits), Hydraulic cylinder casings (after honing), Shaft-type components in mechanical engineering
Application industries: Civil engineering and building construction, Heavy machinery and equipment manufacturing, Offshore and marine engineering (platform modules, helidecks), Bridge construction and repair, Transmission towers and telecommunication masts, Transport and agricultural vehicle chassis, Industrial storage and rack systems, Mining and material handling equipment
EN10219 S355K2H LSAW Steel Pipe Similar / Substitute Material Recommendations
| Country / Region | Standard | Grade | Remarks |
|---|---|---|---|
| European Union | EN 10219-1 | S355J2H | Lower toughness (27 J at -20 °C but only for thickness ≤ 40 mm; K2 guarantees toughness up to 120 mm). J2 may not be equivalent for thick sections. |
| European Union | EN 10219-1 | S355NH | Normalised/normalised rolled fine-grain steel with yield 355 MPa and impact at -20 °C; suitable substitute when normalised condition is acceptable. |
| USA | ASTM A500 / A501 | Grade C | Cold-formed welded structural tubing; minimum yield 345 MPa (slightly lower), impact toughness not typically specified unless by supplementary requirement. |
| USA | API 5L / ISO 3183 | X52 (L360) PSL2 | Pipeline steel with yield 360 MPa and guaranteed toughness at low temperatures; may suit structural pipe applications if geometry compatible. |
| India | IS 4923 | Yst 355 | Hollow sections for structural use; yield 355 MPa, but impact properties may differ unless specifically ordered. |
Notes:
- EN 10219 mandates product analysis and testing specific to each supply condition. Options 1.2 (with Charpy impact properties as per K2) must be specified at the time of enquiry and order.
- LSAW pipes are produced from plate or coil by cold forming and welding. The heat-affected zone may exhibit slightly lower toughness; welding procedure qualification ensures compliance.
- For corrosion protection, S355K2H can be hot-dip galvanised to EN ISO 1461, painted, or metallised. Cold-formed hollow sections are suitable for most post-galvanising processes.
- When ordering, the nominal dimensions (outside diameter or side length, wall thickness) and length should be agreed. Tolerances are per EN 10219-2.
- This material is not intended for pressure purposes unless specifically qualified (e.g., according to EN 13445 or ASME BPVC). For pressure containment, refer to pipe standards such as EN 10217.
- Share



