
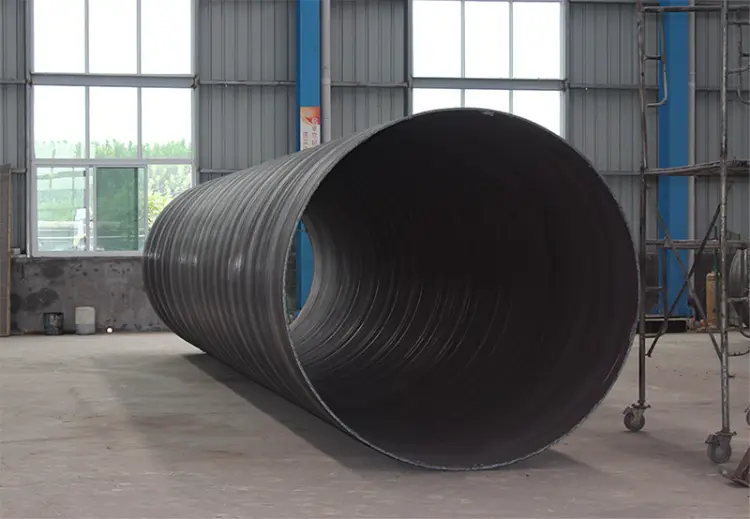
EN10025-6 S500QL Steel for SSAW Pipe
EN10025-6 S500QL Steel for SSAW Pipe - Datasheet & Properties
Complete material data for EN10025-6 S500QL high strength structural steel used in SSAW pipe production: chemical composition, mechanical & physical properties, equivalent grades, and application guide.
Spiral submerged arc welding (SSAW), hot forming (with subsequent heat treatment), machining, cutting, bending
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
EN10025-6 S500QL Steel for SSAW Pipe Introduction
S500QL is a quenched and tempered high yield strength structural steel defined in European standard EN 10025-6. With a minimum yield strength of 500 MPa, it offers an excellent combination of strength, low-temperature toughness (down to -50 °C), and good weldability. The grade is widely used in heavy-duty applications, particularly spiral submerged arc welded (SSAW) pipes for oil and gas transmission, offshore structures, and crane booms.
- High strength – minimum 500 MPa yield
- Low-temperature toughness – designated for -50 °C impact test
- Good weldability – suitable for SSAW pipe manufacturing
- Delivery condition – quenched and tempered (+QT)
EN10025-6 S500QL Steel for SSAW Pipe Chemical Composition
The table below shows the maximum allowable chemical elements according to EN 10025-6:2019 for S500QL. For fine-grain practice, the total aluminium content shall be at least 0.015%. Other microalloying elements may be added to achieve the required strength and toughness.
| Element | Maximum Value (%) | Remarks |
|---|---|---|
| Carbon (C) | 0.20 | |
| Silicon (Si) | 0.80 | |
| Manganese (Mn) | 1.70 | |
| Phosphorus (P) | 0.020 | |
| Sulfur (S) | 0.010 | |
| Nitrogen (N) | 0.015 | |
| Boron (B) | 0.0050 | |
| Chromium (Cr) | 2.0 | |
| Copper (Cu) | 0.50 | |
| Molybdenum (Mo) | 0.70 | |
| Niobium (Nb) | 0.06 | |
| Nickel (Ni) | 2.0 | |
| Titanium (Ti) | 0.05 | |
| Vanadium (V) | 0.12 | |
| Zirconium (Zr) | 0.15 | |
| Aluminium (Al total) | – | ≥ 0.015% for fine-grain practice |
EN10025-6 S500QL Steel for SSAW Pipe Physical & Thermal Properties
The values provided are typical for quenched and tempered medium‑carbon low‑alloy steels and are not mandatory in EN 10025‑6. Actual properties may vary slightly depending on exact composition, heat treatment, and temperature.
| Property | Typical Value | Unit | Conditions |
|---|---|---|---|
| Density (ρ) | 7.85 | g/cm³ | At 20 °C |
| Modulus of elasticity (E) | 210 | GPa | At 20 °C |
| Shear modulus (G) | 80 | GPa | At 20 °C |
| Poisson's ratio (ν) | 0.3 | – | At 20 °C |
| Thermal expansion coefficient (α) | 11.7 × 10⁻⁶ | K⁻¹ | 20–100 °C |
| Thermal expansion coefficient (α) | 12.5 × 10⁻⁶ | K⁻¹ | 20–200 °C |
| Thermal conductivity (λ) | 45 | W/(m·K) | At 20 °C |
| Specific heat capacity (cₚ) | 460 | J/(kg·K) | At 20 °C |
| Electrical resistivity (ρₑ) | 0.25 | μΩ·m | At 20 °C |
EN10025-6 S500QL Steel for SSAW Pipe Mechanical Properties
Minimum values according to EN 10025-6:2019, valid for quenched and tempered condition. Properties depend on product thickness. Impact energy is determined on longitudinal Charpy-V specimens for thicknesses > 10 mm; minimum average value at -50 °C is 27 J. Bending test is performed at room temperature with a mandrel diameter as given.
| Property | Specified Value | Unit | Thickness (t) Condition |
|---|---|---|---|
| Yield strength (ReH) | ≥ 500 | MPa | t ≤ 50 mm |
| Yield strength (ReH) | ≥ 480 | MPa | 50 < t ≤ 100 mm |
| Yield strength (ReH) | ≥ 440 | MPa | 100 < t ≤ 150 mm |
| Tensile strength (Rm) | 590 – 770 | MPa | t ≤ 100 mm |
| Tensile strength (Rm) | 540 – 720 | MPa | 100 < t ≤ 150 mm |
| Elongation (A, L₀=5.65√S₀) | ≥ 17 | % | t ≤ 50 mm |
| Elongation (A, L₀=5.65√S₀) | ≥ 15 | % | 50 < t ≤ 100 mm |
| Elongation (A, L₀=5.65√S₀) | ≥ 15 | % | 100 < t ≤ 150 mm |
| Charpy-V impact energy (KV₂, -50 °C) | ≥ 27 | J | t > 10 mm (longitudinal) |
| Bend test (mandrel diameter) | 2a | – | t ≤ 16 mm |
| Bend test (mandrel diameter) | 3a | – | 16 < t ≤ 50 mm |
| Bend test (mandrel diameter) | 4a | – | 50 < t ≤ 100 mm |
| Bend test (mandrel diameter) | 5a | – | 100 < t ≤ 150 mm |
EN10025-6 S500QL Steel for SSAW Pipe Fully Equivalent Material Standards & Substitutable Grades
| Country / Region | Standard | Grade | Remarks |
|---|---|---|---|
| United Kingdom | BS EN 10025-6 | S500QL | Identical to EN 10025-6 |
| Germany | DIN EN 10025-6 | S500QL | Identical to EN 10025-6 |
| France | NF EN 10025-6 | S500QL | Identical to EN 10025-6 |
| Italy | UNI EN 10025-6 | S500QL | Identical to EN 10025-6 |
| Spain | UNE EN 10025-6 | S500QL | Identical to EN 10025-6 |
EN10025-6 S500QL Steel for SSAW Pipe Application Introduction
S500QL combines high strength with excellent low‑temperature toughness, making it an ideal choice for demanding SSAW pipe applications. The steel is delivered in quenched and tempered condition and can be readily formed into large‑diameter spiral pipes using submerged arc welding.
- Used where weight reduction and high load capacity are required.
- Performs reliably in arctic and offshore environments thanks to guaranteed -50 °C toughness.
- Compatible with standard pipe coating and lining systems.
Product Applications: SSAW pipes for long‑distance pipelines, Structural hollow sections for offshore jackets, Crane booms and lattice structures, Pressure vessel shells, Bridge structural elements
Processed into products: Pipe segments and bends, Flanges and connectors, Welded joints and fittings, Stiffeners and gusset plates, Machined end rings and couplings
Application industries: Oil and gas transmission, Offshore and marine engineering, Construction and infrastructure (bridges, towers), Heavy machinery and transportation, Renewable energy (wind turbine structures)
EN10025-6 S500QL Steel for SSAW Pipe Similar / Comparable Alternative Materials
| Country / Region | Standard | Grade | Remarks |
|---|---|---|---|
| Europe | EN 10025-6 | S500Q | Same strength class, minimum impact temperature 0 °C instead of -50 °C |
| Europe | EN 10025-6 | S500QL1 | Same strength class, minimum impact temperature -20 °C |
| China | GB/T 1591-2018 | Q500D | Comparable yield strength, impact at -20 °C, hot‑rolled or normalised |
| International | ISO 4950‑2:1995 (withdrawn) | E500 | High yield steel, similar strength but different testing regime |
| USA | ASTM A572/A572M | Grade 65 | Yield 450 MPa, lower strength, but widely used in structural pipes |
| Japan | JIS G3128 | SHY685 | Higher strength (690 MPa), for pressure vessels; more alloyed |
Notes:
- Welding: Preheating and post‑weld heat treatment may be required depending on thickness and welding process. Use low‑hydrogen consumables.
- Forming: Hot forming must be followed by a new quenching and tempering treatment to restore the mechanical properties.
- Inspection: Ultrasonic testing (UT) is often required for SSAW pipes; EN 10160 or equivalent NDT standards apply.
- Thickness ranges above 150 mm are not covered in this datasheet; consult the producer for special agreements.
- Share



