
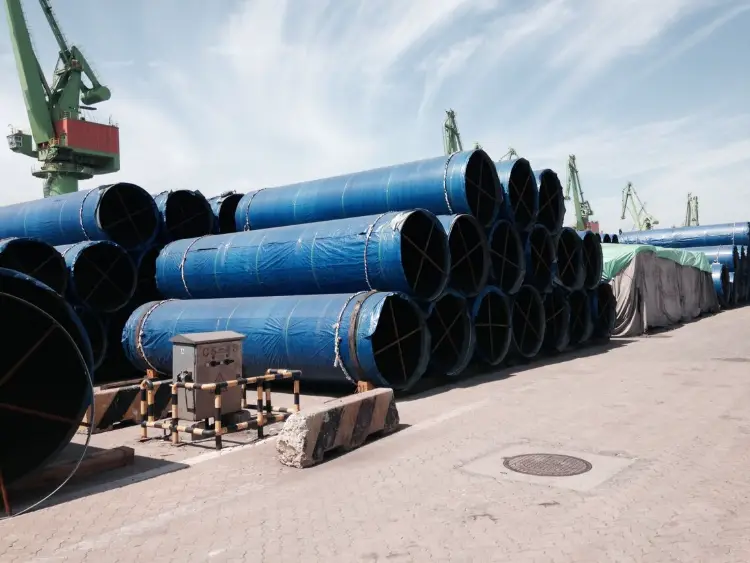
S460QL1 Structural Steel for SSAW Pipe
S460QL1 Structural Steel for SSAW Pipe - EN 10025-6 Q&T High Yield Strength
Comprehensive material data for S460QL1 steel according to EN 10025-6, used in spiral submerged arc welded (SSAW) pipes. Includes chemical composition, mechanical properties, thermal and electrical properties, international equivalents and application guidance.
Hot rolling + quenching and tempering; suitable for cold forming, welding (with preheating and heat input control), machining, SSAW pipe forming
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
S460QL1 Structural Steel for SSAW Pipe Introduction
S460QL1 is a high yield strength structural steel delivered in the quenched and tempered condition, in accordance with EN 10025-6. It offers a minimum yield strength of 460 MPa and excellent low-temperature impact toughness (27 J at -40°C). The 'QL1' designation specifies the improved notch toughness for service at low ambient temperatures. This grade is widely supplied as heavy plates, which are subsequently formed and welded into SSAW (spiral submerged arc welded) pipes for demanding applications such as pressure conduits, offshore structures, and high-strength welded components. The material combines high strength with good weldability, making it suitable for heavy-duty structural and pressure-containing equipment.
S460QL1 Structural Steel for SSAW Pipe Chemical Composition
The chemical composition limits according to EN 10025-6:2019 for grade S460QL1. All values are maximum unless otherwise indicated. Fine grain elements (Nb, V, Ti) may be added singly or in combination. The sum Nb+V+Ti ≤ 0.22% is typically ensured for grain refinement.
- Carbon equivalent (CEV) is usually specified for weldability control; typical CEV ≤ 0.47–0.50 depending on thickness.
| Element | Standard Value (wt%) | Remarks |
|---|---|---|
| Carbon (C) | ≤ 0.20 | |
| Silicon (Si) | ≤ 0.80 | |
| Manganese (Mn) | ≤ 1.70 | |
| Phosphorus (P) | ≤ 0.020 | |
| Sulfur (S) | ≤ 0.010 | |
| Nitrogen (N) | ≤ 0.015 | |
| Boron (B) | ≤ 0.005 | |
| Chromium (Cr) | ≤ 1.50 | |
| Copper (Cu) | ≤ 0.50 | |
| Molybdenum (Mo) | ≤ 0.70 | |
| Niobium (Nb) | ≤ 0.06 | |
| Nickel (Ni) | ≤ 2.0 | |
| Titanium (Ti) | ≤ 0.05 | |
| Vanadium (V) | ≤ 0.12 | |
| Zirconium (Zr) | ≤ 0.15 | |
| Sum of Nb+V+Ti | ≤ 0.22 | Fine grain element combination |
S460QL1 Structural Steel for SSAW Pipe Thermal and Electrical Properties
The following physical property data are typical for quenched and tempered structural steel similar to S460QL1. They are not specified in EN 10025-6 but are provided for engineering calculations. Values may vary slightly depending on exact chemical composition and heat treatment.
- Thermal conductivity and expansion data are given for common temperature ranges.
- Electrical resistivity is given for 20 °C.
| Property | Typical Value | Unit | Condition / Temperature |
|---|---|---|---|
| Density (ρ) | 7850 | kg/m³ | 20 °C |
| Modulus of elasticity (E) | 210 | GPa | 20 °C |
| Shear modulus (G) | 81 | GPa | 20 °C (estimated) |
| Poisson's ratio (ν) | 0.3 | – | 20 °C |
| Thermal expansion coefficient (α) | 11.1 × 10⁻⁶ | K⁻¹ | 20 – 100 °C |
| Thermal expansion coefficient (α) | 12.1 × 10⁻⁶ | K⁻¹ | 20 – 200 °C |
| Thermal expansion coefficient (α) | 13.0 × 10⁻⁶ | K⁻¹ | 20 – 400 °C |
| Thermal conductivity (λ) | 50 | W/(m·K) | 20 °C |
| Thermal conductivity (λ) | 47 | W/(m·K) | 200 °C |
| Thermal conductivity (λ) | 42 | W/(m·K) | 400 °C |
| Specific heat capacity (c) | 460 | J/(kg·K) | 20 °C |
| Specific heat capacity (c) | 530 | J/(kg·K) | 200 °C |
| Electrical resistivity (ρ_e) | 0.20 × 10⁻⁶ | Ω·m | 20 °C (typical low-alloy steel) |
S460QL1 Structural Steel for SSAW Pipe Mechanical Properties
Mechanical properties at room temperature according to EN 10025-6 for plate thickness ≤50 mm, unless other thickness ranges are indicated. Transverse tensile specimens are standard; elongation measured on proportional gauge length (5.65√S₀). Impact tests are performed on Charpy V-notch longitudinal specimens.
- Properties for SSAW pipe may be influenced by forming and welding; values refer to the parent plate material.
| Property | Value | Unit | Test Condition |
|---|---|---|---|
| Yield strength (ReH) | ≥ 460 | MPa | t ≤ 50 mm, transverse |
| Yield strength (ReH) | ≥ 440 | MPa | 50 < t ≤ 100 mm, transverse |
| Tensile strength (Rm) | 550 – 720 | MPa | t ≤ 50 mm, transverse |
| Tensile strength (Rm) | 550 – 720 | MPa | 50 < t ≤ 100 mm, transverse |
| Elongation after fracture (A) | ≥ 17 | % | t ≤ 50 mm, gauge length 5.65√S₀, transverse |
| Elongation after fracture (A) | ≥ 17 | % | 50 < t ≤ 100 mm, gauge length 5.65√S₀, transverse |
| Bend test (mandrel diameter) | 3 t | – | t ≤ 16 mm, 180° bend |
| Bend test (mandrel diameter) | 4 t | – | 16 < t ≤ 50 mm, 180° bend |
| Impact energy (KV) | ≥ 27 | J | -40 °C, Charpy V, longitudinal |
S460QL1 Structural Steel for SSAW Pipe Exact Equivalent Material Standards & Recommended Substitute Grades
| Country / Region | Standard | Grade | Remarks |
|---|---|---|---|
| European Union | EN 10025-6 | S460QL1 | Original standard; direct use for SSAW pipe |
| Germany | DIN EN 10025-6 | S460QL1 | Identical adoption of European standard |
| United Kingdom | BS EN 10025-6 | S460QL1 | Identical; formerly BS 4360 superseded |
| International (ISO) | ISO 4950-2:1995 (withdrawn) | E460DD | Historically similar; not a direct current equivalent |
S460QL1 Structural Steel for SSAW Pipe Application Introduction
S460QL1 steel is primarily used in the construction of high-strength welded structures, particularly spiral submerged arc welded (SSAW) pipes. Plates meeting this specification are formed into cylindrical pipes by spiral welding, providing efficient use of material for large-diameter, thick-walled pipes. Its excellent low-temperature toughness makes it suitable for demanding environments such as arctic service or high-pressure gas pipelines.
- The combination of high strength and good weldability reduces plate thickness and overall weight in structural applications.
- Post-weld heat treatment is generally not required for standard thicknesses, but may be necessary for very heavy sections to relieve residual stresses.
Product Applications: SSAW pipes for long-distance high-pressure gas/oil pipelines, Pressure vessels and storage tanks (welded from plates), Offshore platform tubular members and nodes, Crane jibs and booms, Structural beams and girders, Piling pipes and foundation elements
Processed into products: Spiral welded pipe spools and fittings, Flanges and end caps for pressure piping, Welded sandwich panels for heavy-duty structures, Tubular connectors and transition pieces, Reinforcement pads and stiffeners, Machined parts from Q&T plate (e.g., bearing plates, end connections)
Application industries: Oil and gas transmission (high-strength pipelines), Offshore and marine engineering (jackets, risers, subsea structures), Pressure vessel and boiler manufacturing, Hydraulic and hydropower engineering (penstocks, spiral casing), Heavy machinery and crane construction, Bridge building (structural sections)
S460QL1 Structural Steel for SSAW Pipe Similar / Closely Related Substitute Materials
| Country / Region | Standard | Grade | Remarks |
|---|---|---|---|
| European Union | EN 10025-6 | S460Q | Same Q&T condition but impact tested at 0°C („Q"); good alternative for less severe low-temperature service |
| European Union | EN 10025-6 | S460QL | Q&T with impact tested at -20°C („QL"); slightly lower toughness than QL1 |
| European Union | EN 10025-4 | S460M | Thermomechanical rolled (M); similar minimum strength but no quench/temper; impact properties may differ |
| European Union | EN 10025-3 | S460N | Normalized (N); similar strength with good toughness; not identical welding or strength behavior |
| USA | ASTM A572 / A709 | Grade 65 / HPS 70W | Comparable yield strength; different production route and toughness specification; verify welding procedures |
Notes:
Remark on SSAW pipe manufacturing: The material data provided are for the base plate steel S460QL1 according to EN 10025-6. When fabricated into spiral welded pipes, the pipe may be subject to additional norms (e.g., API 5L, ISO 3183) which may impose supplementary requirements on chemistry, mechanical properties, and non-destructive testing. The minimum longitudinal yield strength of the pipe may be slightly lower than the transverse plate properties due to the Bauschinger effect during cold forming; the pipe manufacturer typically accounts for this by selecting appropriate plate grades and wall thickness.
Welding consumables should match the strength and toughness requirements of S460QL1. Preheating and interpass temperature control are recommended depending on thickness and CEV. The CEV according to EN 10025-6 usually ranges from 0.44 to 0.53 for this grade; a specific CEV max may be agreed upon to ensure weldability.
Delivery conditions for SSAW pipe may include as-welded, stress-relieved, or with additional coating (external 3LPE/3LPP, internal epoxy) according to project specifications.
- Share



