
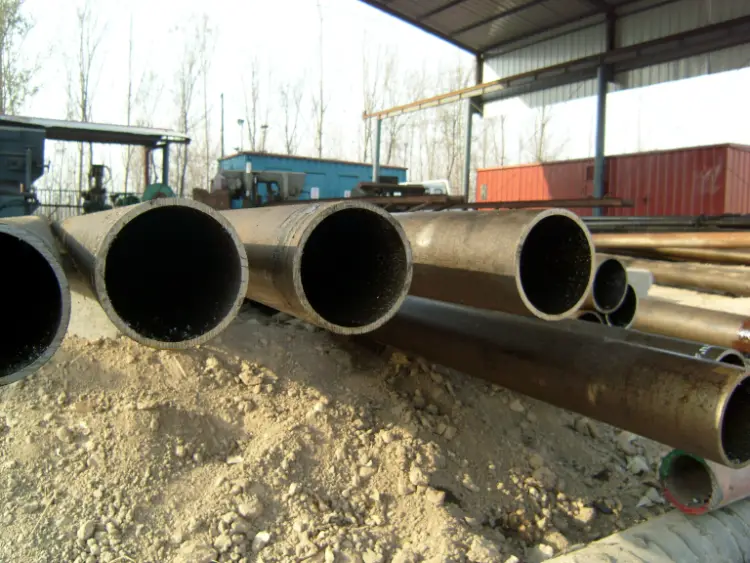
EN 10025-6 S550QL1 SSAW Pipe
EN 10025-6 S550QL1 SSAW Pipe - High Strength Quenched & Tempered Steel Data
Technical data for S550QL1 steel grade according to EN 10025-6 used for spiral submerged arc welded (SSAW) pipes, including chemical composition, mechanical properties, physical parameters, and equivalent grades.
Cutting, cold forming, hot forming, welding, bending
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
EN 10025-6 S550QL1 SSAW Pipe Introduction
S550QL1 is a high-strength, quenched and tempered structural steel defined in EN 10025-6. It offers a minimum yield strength of 550 MPa for thicknesses up to 50 mm and excellent notch toughness down to -60°C (L1 category), making it ideal for demanding welded tubular applications.
- Excellent low-temperature impact toughness
- High strength-to-weight ratio
- Good weldability with appropriate precautions
- Available as plates, strips, and hollow sections for SSAW pipe production
EN 10025-6 S550QL1 SSAW Pipe Chemical Composition
Composition limits according to EN 10025-6:2019 for grade S550QL1. All values are maximum unless otherwise stated. The steel is fully killed with fine grain practice. Alloying elements are adjusted to achieve the required mechanical properties and weldability.
| Element | Standard Value (max %) | Remarks |
|---|---|---|
| Carbon (C) | 0.20 | |
| Silicon (Si) | 0.80 | |
| Manganese (Mn) | 1.70 | |
| Phosphorus (P) | 0.020 | |
| Sulfur (S) | 0.010 | |
| Chromium (Cr) | 1.50 | |
| Nickel (Ni) | 2.00 | |
| Molybdenum (Mo) | 0.70 | |
| Vanadium (V) | 0.12 | |
| Titanium (Ti) | 0.05 | |
| Niobium (Nb) | 0.06 | |
| Nitrogen (N) | 0.015 | |
| Boron (B) | 0.005 | |
| Zirconium (Zr) | 0.15 | |
| Copper (Cu) | 0.50 | |
| *Aluminium (Al) | ≥ 0.015 (total) | Sufficient total aluminium if present |
EN 10025-6 S550QL1 SSAW Pipe Thermal & Electrical Physical Properties
Typical physical properties for tempered low-alloy carbon steels. These values are not specified in EN 10025-6 but are representative for engineering calculations at room temperature unless another condition is indicated. Variations may occur depending on actual chemical composition and heat treatment.
| Property | Typical Value | Unit | Test Condition / Remarks |
|---|---|---|---|
| Density (ρ) | 7850 | kg/m³ | At 20 °C |
| Modulus of elasticity (E) | 210 | GPa | At 20 °C |
| Shear modulus (G) | 81 | GPa | Calculated from E and ν |
| Poisson's ratio (ν) | 0.3 | – | Elastic range |
| Thermal expansion coefficient (α) | 11.1 × 10⁻⁶ | 1/K | 20 – 100 °C |
| Thermal expansion coefficient (α) | 12.1 × 10⁻⁶ | 1/K | 20 – 200 °C |
| Thermal expansion coefficient (α) | 12.9 × 10⁻⁶ | 1/K | 20 – 300 °C |
| Thermal expansion coefficient (α) | 13.5 × 10⁻⁶ | 1/K | 20 – 400 °C |
| Thermal expansion coefficient (α) | 13.9 × 10⁻⁶ | 1/K | 20 – 500 °C |
| Thermal conductivity (λ) | 42 | W/(m·K) | At 20 °C |
| Thermal conductivity (λ) | 45 | W/(m·K) | At 100 °C |
| Thermal conductivity (λ) | 42 | W/(m·K) | At 200 °C |
| Thermal conductivity (λ) | 38 | W/(m·K) | At 300 °C |
| Specific heat capacity (c) | 460 | J/(kg·K) | 20 – 100 °C |
| Electrical resistivity (ρ_e) | 0.25 | µΩ·m | At 20 °C |
EN 10025-6 S550QL1 SSAW Pipe Mechanical Properties
Minimum requirements as per EN 10025-6 for S550QL1. Properties depend on product thickness. Values are applicable to the supplied condition (+QT). For SSAW pipes, testing is conducted on the base material from the mother plate/coil; weld zone properties are validated separately.
| Property | Required Value | Unit | Test Condition / Thickness |
|---|---|---|---|
| Yield Strength (ReH) | ≥ 550 | MPa | t ≤ 50 mm |
| Yield Strength (ReH) | ≥ 530 | MPa | 50 < t ≤ 100 mm |
| Yield Strength (ReH) | ≥ 500 | MPa | 100 < t ≤ 150 mm |
| Tensile Strength (Rm) | 640 – 820 | MPa | t ≤ 50 mm |
| Tensile Strength (Rm) | 590 – 770 | MPa | 50 < t ≤ 100 mm |
| Tensile Strength (Rm) | 590 – 770 | MPa | 100 < t ≤ 150 mm |
| Elongation after fracture (A) | ≥ 16 | % | Longitudinal; t ≤ 50 mm |
| Elongation after fracture (A) | ≥ 16 | % | Longitudinal; 50 < t ≤ 100 mm |
| Elongation after fracture (A) | ≥ 16 | % | Longitudinal; 100 < t ≤ 150 mm |
| Charpy V-notch impact (KV₂) | ≥ 27 | J | Longitudinal; -60 °C (L1) |
| Bend test 180° (d = mandrel diameter) | d = 3 t | – | t ≤ 16 mm |
| Bend test 180° | d = 4 t | – | 16 < t ≤ 50 mm |
| Bend test 180° | d = 5 t | – | 50 < t ≤ 80 mm |
| Bend test 180° | d = 6 t | – | 80 < t ≤ 150 mm |
EN 10025-6 S550QL1 SSAW Pipe Completely Equivalent Standards and Designations
| Country / Region | Standard | Designation | Remarks |
|---|---|---|---|
| Germany | DIN EN 10025-6 | S550QL1 | Identical to EN 10025-6 |
| United Kingdom | BS EN 10025-6 | S550QL1 | Identical to EN 10025-6 |
| France | NF EN 10025-6 | S550QL1 | Identical to EN 10025-6 |
| Italy | UNI EN 10025-6 | S550QL1 | Identical to EN 10025-6 |
| Spain | UNE EN 10025-6 | S550QL1 | Identical to EN 10025-6 |
| Belgium | NBN EN 10025-6 | S550QL1 | Identical to EN 10025-6 |
| Netherlands | NEN EN 10025-6 | S550QL1 | Identical to EN 10025-6 |
| Sweden | SS EN 10025-6 | S550QL1 | Identical to EN 10025-6 |
| Poland | PN EN 10025-6 | S550QL1 | Identical to EN 10025-6 |
EN 10025-6 S550QL1 SSAW Pipe Application Introduction
S550QL1 is widely applied in sectors requiring high reliability under extreme conditions, especially where low-temperature toughness is critical.
- Offshore & Marine: Jacket legs, conductor pipes, riser components.
- Civil Engineering: Foundation piles (SSAW pipes), bridge piers, structural columns.
- Energy Sector: Wind turbine tower sections, penstocks, cryogenic storage.
- Mining & Heavy Machinery: Crane booms, excavator arms, heavy-duty transport chassis.
Product Applications: Spiral submerged arc welded (SSAW) pipes for piling and structural use, Longitudinal welded heavy-wall pipes for hydrocarbon transport, Jack-up rig legs and spudcans, Transition pieces and monopiles for offshore wind turbines, Hydraulic cylinder bodies subjected to high stress, Crane lattice booms and crawler crane components
Processed into products: SSAW pipe joints with machined end preparations for welding, Structural tubular nodes and gusset plates for jacket frames, Thick-walled hollow sections for telescopic crane extensions, Machined shafts and pins for heavy machinery, Welded tubular connectors for offshore risers, Flanged pipe spools for high-pressure penstocks
Application industries: Offshore oil & gas platforms and subsea structures, Renewable energy (wind turbine towers and foundations), Heavy construction and infrastructure (bridges, high-rise buildings), Marine engineering (shipbuilding, port equipment), Mining and earthmoving machinery, Pressure vessel and cryogenic equipment manufacturing, SSAW pipe production for piling and water supply
EN 10025-6 S550QL1 SSAW Pipe Closely Related / Substitute Steel Grades
| Country / Region | Standard | Designation | Remarks |
|---|---|---|---|
| EU | EN 10025-6 | S550QL | Similar quenched & tempered steel; impact tested at -40°C instead of -60°C |
| EU | EN 10025-6 | S550Q | Same strength level without mandatory low-temperature toughness requirement |
| EU | EN 10025-6 | S620QL1 | Higher yield strength (620 MPa) with -60°C impact; can be used when greater strength is required |
| EU | EN 10025-6 | S500QL1 | Slightly lower yield strength (500 MPa) but same toughness; may be acceptable for less demanding designs |
| USA | ASTM A514/A514M | Grade B (690 MPa) | Higher strength Q&T steel; not directly equivalent but sometimes used in heavy construction; different composition approach |
| USA | ASTM A517/A517M | Grade B (690 MPa) | Similar to A514 but intended for pressure vessel applications; requires careful qualification for substitution |
Notes:
Manufacturing SSAW pipes: The steel is supplied as hot-rolled coils or plates. Spiral forming is followed by double submerged arc welding. Post-weld heat treatment (PWHT) may be specified to relieve residual stresses. Welding procedures must be qualified according to ISO 15614-1 or equivalent; low-hydrogen practices are essential to avoid cold cracking. The L1 designation guarantees adequate notch toughness at service temperatures down to -60°C, which is crucial for Arctic applications. NDT of the weld seam (ultrasonic or radiographic) is normally mandatory. Contact standard EN 10225 for offshore structural steel if more detailed weldability criteria or CTOD testing are needed.
- Share



