
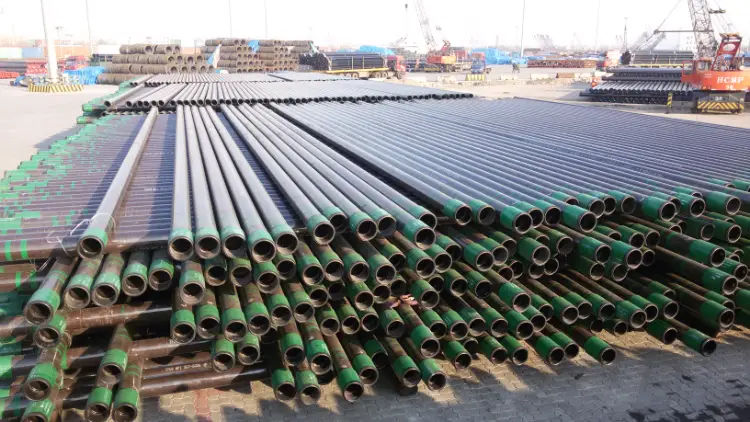
API 5L X80 PSL2 SSAW Pipe
API 5L X80 PSL2 SSAW Pipe: High-Strength Steel for Critical Pipeline Transport
Comprehensive material data for API 5L X80 PSL2 SSAW pipe, including chemical composition, mechanical properties, thermal and electrical characteristics.
Hot-rolled plate/skelp → spiral forming → double-sided SSAW welding → post-weld heat treatment (if required) → expansion and testing
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
API 5L X80 PSL2 SSAW Pipe Introduction
API 5L X80 PSL2 is a high-strength, low-alloy (HSLA) steel grade designed for longitudinal or spiral submerged-arc welded (SSAW) line pipes used in oil and gas transmission systems. As per API Specification 5L, this grade belongs to PSL 2 (Product Specification Level 2), which imposes stricter requirements on chemical composition, fracture toughness, and non-destructive testing compared to PSL 1. X80 offers a minimum yield strength of 555 MPa (80,500 psi) and excellent weldability, making it suitable for demanding high-pressure, long-distance pipelines. The SSAW forming process enables cost-effective manufacturing of large-diameter pipes. Typical applications include onshore and offshore gas and oil transportation, where strength, ductility, and resistance to fracture propagation are critical.
API 5L X80 PSL2 SSAW Pipe Chemical Composition
Chemical composition requirements according to API 5L Table 3A for PSL 2 pipe with t ≤ 25.0 mm (1 in). Elements like Nb, V, Ti may be added individually or in combination for grain refinement and strengthening. Carbon equivalent (CEIIW) maximum is typically 0.43% for X80, but may be specified by purchaser.
| Chemical Element | Specified Value (max, %) | Remarks |
|---|---|---|
| Carbon (C) | 0.12 | Heat analysis |
| Manganese (Mn) | 1.85 | Maximum for t ≤ 25.0 mm |
| Phosphorus (P) | 0.025 | |
| Sulfur (S) | 0.015 | |
| Silicon (Si) | 0.45 | |
| Vanadium (V) | 0.06 | V + Nb + Ti ≤ 0.15% |
| Niobium (Nb) | 0.06 | V + Nb + Ti ≤ 0.15% |
| Titanium (Ti) | 0.06 | V + Nb + Ti ≤ 0.15% |
| Copper (Cu) | 0.50 | |
| Nickel (Ni) | 0.50 | |
| Chromium (Cr) | 0.50 | |
| Molybdenum (Mo) | 0.50 | |
| Boron (B) | 0.0005 | If intentionally added |
| Aluminum (Al) | 0.060 | Total aluminum |
| Nitrogen (N) | 0.012 | |
| Carbon Equivalent (CEIIW) | Typically 0.43 max | May be agreed between purchaser and manufacturer |
API 5L X80 PSL2 SSAW Pipe Thermal & Electrical Physical Properties
Typical physical properties for API 5L X80 steel at room temperature. These values are representative for low-carbon microalloyed pipeline steel and may vary slightly with exact composition and manufacturing process. They are provided for engineering reference but are not part of API 5L mandatory requirements.
| Property | Typical Value | Unit | Test Condition |
|---|---|---|---|
| Density (ρ) | 7.85 | g/cm³ | 20°C |
| Elastic modulus (E) | 210 | GPa | 20°C, tension |
| Shear modulus (G) | 81 | GPa | Calculated from E and ν |
| Poisson's ratio (ν) | 0.3 | - | 20°C |
| Thermal expansion coefficient (α) | 11.7 | 10⁻⁶/K | 20°C to 100°C |
| Thermal conductivity (λ) | 50 | W/(m·K) | 20°C |
| Specific heat capacity (cp) | 480 | J/(kg·K) | 20°C |
| Electrical resistivity (ρe) | 0.20 | 10⁻⁶ Ω·m | 20°C |
API 5L X80 PSL2 SSAW Pipe Mechanical Properties
Mechanical properties according to API 5L Table 6 for PSL 2 pipe. Transverse tensile properties are applicable for welded pipe. The yield strength is specified as the minimum for the 0.5% total extension under load or 0.2% offset. Impact test requirements depend on pipe size and wall thickness, often performed at -20°C or lower as per supplementary requirements.
| Property | Specified Value | Unit | Test Condition |
|---|---|---|---|
| Yield Strength (Rt0.5 or Rp0.2) | 555 - 705 | MPa | Transverse specimen, room temperature |
| Tensile Strength (Rm) | 625 - 825 | MPa | Transverse specimen, room temperature |
| Yield/Tensile Ratio (Rt0.5/Rm) | 0.93 max | - | As per various supplementary requirements |
| Elongation after fracture (Af) | Calculated per API 5L: e.g., min 22% for t ≤ 20 mm | % | Gauge length 2 in or 50 mm; formula: Af = 1950 * (Axc0.2) / UTS0.9 |
| Charpy V-notch impact energy (base metal) | ≥ 27 J (average), ≥ 20 J (single) | J | At -20°C or lower; transverse specimens, 10x10 mm |
| Bend test (180°) | No cracks or defects | - | Bend diameter per standard; typically 3t for thickness ≤12.5 mm |
| Hardness (base metal & HAZ) | 250 HV10 or 22 HRC max | - | Sour service supplementary requirements |
API 5L X80 PSL2 SSAW Pipe Exact Equivalent Material Standards & Replaceable Grades
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| International | ISO 3183 | L555M or L555MB | M = thermomechanically rolled; MB = thermomechanically rolled + accelerated cooled |
| Europe | EN 10208-2 | L555MB | Pipe for pipelines for combustible fluids |
| China | GB/T 9711 | L555 | PSL2 requirements aligned with ISO 3183 |
| Canada | CAN/CSA Z245.1 | Category II 550 | Also covers yield strength 550 MPa, but can be ordered as 555 |
| Russia | GOST ISO 3183 | K60 (if yield ~555 MPa) | Adopted ISO standard |
API 5L X80 PSL2 SSAW Pipe Application Introduction
API 5L X80 PSL2 SSAW pipe is widely adopted in high-strain and high-pressure pipeline systems due to its balance between strength, toughness, and cost-effectiveness via spiral welding. Typical application guidance includes:
Product Applications: Long-distance cross-country gas transmission pipelines, High-pressure oil trunk lines, Gathering and distribution networks, Offshore risers and flowlines, Station piping for compressor and pumping stations
Processed into products: Line pipe segments (12 m or 24 m lengths), Bends, elbows, and tees (induction hot-formed), Flanges and mechanical connectors (matching material), Cold-expanded pipes for reeling applications, Insulated pipe-in-pipe systems
Application industries: Oil and gas upstream and midstream transportation, Petrochemical and refining, Power generation (cooling water, steam lines), Water and slurry transport (large-diameter lines), Offshore and subsea pipeline systems
API 5L X80 PSL2 SSAW Pipe Similar or Alternative Material Recommendations
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| USA / International | API 5L PSL2 | X70 (L485) | Lower strength, often used when X80 is not required; better availability |
| USA / International | API 5L PSL2 | X80 (L555) PSL1 | Same strength level but less stringent quality requirements; not for critical applications |
| International | ISO 3183 | L550M (X80) | Yield min 550 MPa, slightly lower than X80 (555 MPa) |
| Offshore Application | DNVGL-ST-F101 (DNV OS-F101) | S420 (for sour) or S450 | Supplements for submarine pipelines; adjusted matching to X80 strength |
| Europe | EN 10208-2 | L550MB | Yield minimum 550 MPa |
Notes:
Additional requirements: PSL 2 orders may include supplementary demands such as
- Hydrogen Induced Cracking (HIC) and Sulfide Stress Cracking (SSC) testing for sour service (NACE MR0175/ISO 15156).
- Dual-grade certification to both API 5L and ISO 3183.
- Post-weld heat treatment (PWHT) for heavy-wall pipe.
- Strain-based design with enhanced longitudinal tensile properties.
- Alternative chemical analyses with lower carbon or alloy to meet CEQ limits.
All welds shall be 100% inspected by ultrasonic or radiographic testing. The information provided represents standard requirements; actual values may be tightened per project specification.
- Share



