
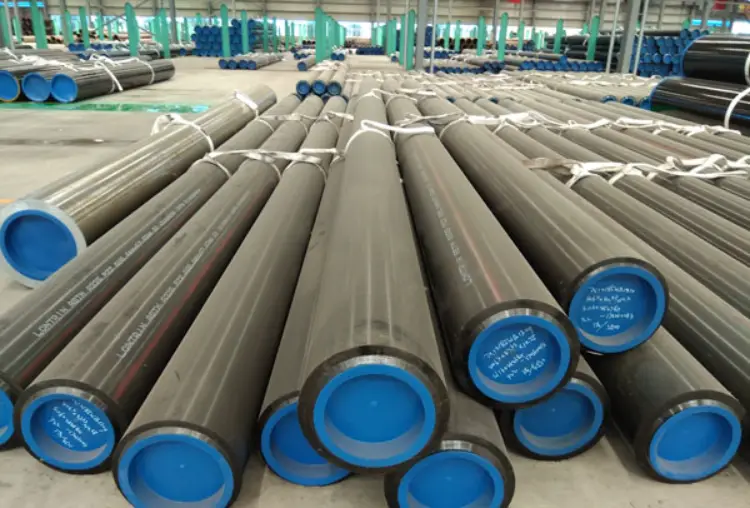
API 5L PSL2 X60 LSAW Pipe
API 5L X60 PSL2 LSAW Pipe: High-Strength Steel for Critical Pipeline Applications
Comprehensive data sheet for API 5L X60 PSL2 LSAW steel pipe covering chemical composition, mechanical properties, thermal and electrical physical performance, and equivalent grades for oil & gas transportation.
Thermo-mechanical controlled rolling (TMCP), normalizing, or quenching and tempering; pipe forming and welding; post-weld heat treatment may be applied
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
API 5L PSL2 X60 LSAW Pipe Introduction
API 5L X60 PSL2 LSAW pipe is a high-strength low-alloy (HSLA) steel line pipe manufactured by longitudinal submerged arc welding under the API 5L specification, Product Specification Level 2 (PSL2). With a specified minimum yield strength of 60 ksi (415 MPa), it offers an optimized balance of strength, toughness, and weldability. LSAW (Longitudinal Submerged Arc Welded) technology enables the production of large-diameter, thick-walled pipes suitable for high-pressure transmission of oil, gas, and water over long distances. PSL2 imposes stricter chemical composition limits, mandatory notch toughness testing, and more comprehensive non-destructive inspection compared to PSL1, ensuring superior reliability in demanding environments.
API 5L PSL2 X60 LSAW Pipe Chemical Composition according to API 5L PSL2
Chemical composition requirements for API 5L X60 PSL2 line pipe, based on API 5L standard. Maximum allowable values are given for heat analysis. Carbon equivalent (CEIIW and CEPcm) limits apply for weldability control
- CEIIW ≤ 0.43% typical for X60
- CEPcm ≤ 0.25% typical
. Note: alloying elements like Nb, V, Ti are added for grain refinement and strengthening but individual limits are not specified; product analysis limits are slightly relaxed.
| Element | Composition (max, %) | Remarks |
|---|---|---|
| Carbon (C) | 0.26 | For carbon content >0.12%, CE limits apply |
| Manganese (Mn) | 1.40 | Higher Mn may be used if CE limits are met |
| Phosphorus (P) | 0.030 | For PSL2 |
| Sulfur (S) | 0.030 | For PSL2 |
| Silicon (Si) | Not specified | Typically 0.15–0.45% for deoxidation |
| Niobium (Nb) | Not specified | Microalloying, typical ≤0.05% |
| Vanadium (V) | Not specified | Microalloying, typical ≤0.10% |
| Titanium (Ti) | Not specified | Microalloying, typical ≤0.06% |
| Nickel (Ni) | Not specified | Allowable residual ≤0.50% max unless agreed |
| Chromium (Cr) | Not specified | Allowable residual ≤0.50% max unless agreed |
| Molybdenum (Mo) | Not specified | Allowable residual ≤0.50% max unless agreed |
| Copper (Cu) | Not specified | Allowable residual ≤0.50% max unless agreed |
API 5L PSL2 X60 LSAW Pipe Thermal and Electrical Physical Properties
Typical physical properties for API 5L X60 grade steel at room temperature. These values are not part of the mandatory API 5L specification but are provided for design calculations. Values are representative for low-alloy steel with ferrite-pearlite microstructure.
| Property | Typical Value | Unit | Test Condition / Remarks |
|---|---|---|---|
| Density (ρ) | 7850 | kg/m³ | At 20°C |
| Elastic Modulus (E) | 205 | GPa | At 20°C; for elevated temperature, use reduction factors |
| Shear Modulus (G) | 80 | GPa | Calculated from E and ν |
| Poisson's Ratio (ν) | 0.30 | - | At 20°C |
| Thermal Expansion Coefficient (α) | 11.7 | 10⁻⁶/K | At 20–100°C; increases with temperature (≈12.5 at 20–300°C) |
| Thermal Conductivity (λ) | 50 | W/(m·K) | At 20°C; decreases with increasing temperature |
| Specific Heat Capacity | 480 | J/(kg·K) | At 20°C; increases with temperature |
| Electrical Resistivity (ρ_e) | 0.20 | µΩ·m | At 20°C |
API 5L PSL2 X60 LSAW Pipe Mechanical Properties of API 5L X60 PSL2 LSAW Pipe
Tensile and toughness requirements for pipe body and weld seam per API 5L. PSL2 requires notch toughness testing (Charpy V-notch) at specified temperatures. The table below shows typical specified values for pipe body. Weld seam tensile strength must be at least the same minimum as the pipe body. Flattening and guided bend tests are mandatory for welded pipes.
| Property | Specified Value | Unit | Test Condition / Remarks |
|---|---|---|---|
| Yield Strength (Rt0.5) | 415–565 | MPa | Transverse or longitudinal as agreed; ≤0.93 tensile strength ratio |
| Tensile Strength (Rm) | 520–760 | MPa | Transverse or longitudinal as agreed |
| Elongation (A) | ≥ 19 | % | Based on 50 mm gauge length, transverse; calculated minimum by formula: Af = C * A xc ^0.2 / UTS ^0.9 (see standard) |
| Yield to Tensile Ratio (Rt0.5/Rm) | ≤ 0.93 | - | Mandatory for PSL2 |
| Charpy V-Notch (KV) | ≥ 27 (average of 3) | J | Minimum single value 20 J; test temperature as per specification (often -10°C, -20°C, or lower) |
| Shear Area (for DWTT if required) | ≥ 80-85 | % | At specified temperature for ductile fracture pipe must meet supplementary requirements |
| Hardness | ≤ 250 HV10 or ≤ 22 HRC | - | For PSL2, maximum hardness limit applies to weld and HAZ |
API 5L PSL2 X60 LSAW Pipe Completely Equivalent Material Standards and Substitutable Grades
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| Europe | EN 10208-2 | L415MB (formerly L415NB/L415QB) | Full equivalence for PSL2, option with B, M, Q indicating delivery condition |
| International (ISO) | ISO 3183 | L415 (PSL2) | Direct adoption of API 5L; L415 designates min yield 415 MPa |
| China | GB/T 9711 | L415 (PSL2) | Equivalent to API 5L X60 line pipe |
| Canada | CSA Z245.1 | Grade 415 (Category II or III) | Matches X60 PSL2 requirements |
| Russia / CIS | GOST R 52079 | K60 (К60) | Similar strength class, with minor difference in test requirements |
| Brazil | ABNT NBR 15273 | X60 | Adopted from API 5L |
API 5L PSL2 X60 LSAW Pipe Application Introduction
API 5L X60 PSL2 LSAW pipe is primarily intended for high-pressure transmission of natural gas, crude oil, and petroleum products. Its high strength and notch toughness make it suitable for long-distance onshore pipelines, offshore risers, and sour service if specially tested (HIC/SSC). LSAW pipe with large diameter (up to 56'' and more) and heavy wall thickness is employed in trunk lines, compressor station piping, and river crossings. The material can be easily welded using standard procedures (SMAW, GMAW, SAW) and can be cold bent to a certain radius.
Product Applications: Onshore transmission pipelines (cross-country pipelines), Offshore pipelines (seabed lines, risers), Flowlines and gathering lines, Compressor station and pumping station piping, Water injection and disposal lines, Piling pipes for jetties and bridges, Conductor casings for oil & gas wells
Processed into products: Line pipe spools and fittings (bends, tees, reducers), Flanged connections and manifolds, Pipeline valves bodies (when forged from equivalent grade), Hot induction bends, Structural tubulars (legs, braces) for offshore platforms, Thrust bores and casing pipes, Anchor flanges for pipeline restraint
Application industries: Oil and Gas Exploration and Production, Pipeline Transportation (Crude Oil, Natural Gas, Refined Products), Water Transmission and Distribution, Slurry and Mining, Structural and Civil Engineering (Piling, Jackets), Geothermal Projects
API 5L PSL2 X60 LSAW Pipe Near-Equivalent or Similar Alternative Grades
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| USA / International | API 5L PSL2 | X65 (L450) | Slightly higher yield strength (450 MPa); can substitute X60 with design recalculation |
| USA / International | API 5L PSL2 | X56 (L390) | Slightly lower strength; might be used in lower pressure applications |
| Europe | EN 10208-2 | L450MB | Next higher strength grade, fully weldable and tough |
| Europe | EN 10208-2 | L415NB | Normalized condition, similar properties but with full-killed fine grain structure |
| Europe | EN 10025-3 | S420N/S420NL | Structural steel normalizing rolled, might substitute for non-pipeline structural use |
| International | ASTM A572 / A572M | Grade 60 [415] | HSLA structural steel, similar yield strength, for non-pipeline structural applications |
| China | GB/T 1591 | Q420 (Q420C,D,E) | Low alloy high strength structural steel, yield ~420 MPa, for structural purposes |
Notes:
- PSL2 requirements include mandatory Charpy V-notch tests, weld seam toughness, hydrogen-induced cracking (HIC) and sulfide stress cracking (SSC) tests may be required by supplementary order for sour service applications.
- Maximum carbon equivalent limits: typically CEIIW ≤ 0.43% and CEPcm ≤ 0.25% for X60, to ensure good weldability.
- LSAW pipe is produced by forming plate into a cylinder and welding the longitudinal seam using submerged arc welding; commonly available in diameters from 16" to 64" (406 mm to 1626 mm) and wall thicknesses up to 50 mm.
- Stringent dimensional tolerances apply to diameter, ovality, wall thickness, and straightness per API 5L.
- Share



