
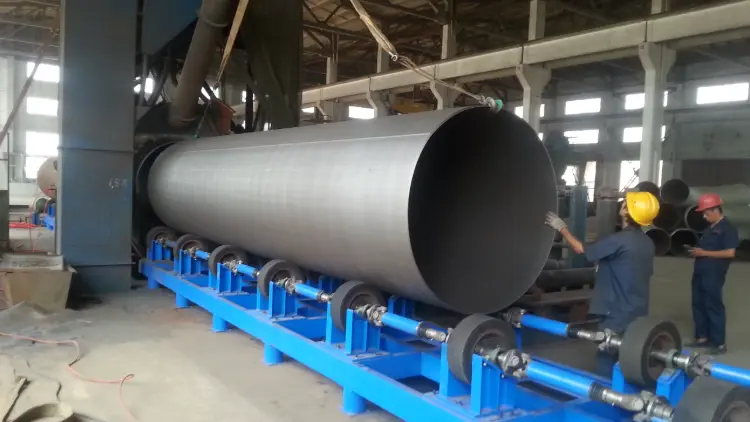
EN10025-2 S235J0 Steel for SSAW Pipe
EN10025-2 S235J0 Steel for SSAW Pipe: Chemical, Mechanical & Physical Properties
Comprehensive analysis of S235J0 steel according to EN10025-2, used for spiral submerged arc welded (SSAW) pipes. Includes chemical composition, mechanical properties, physical properties, international equivalents, and application guidance.
Hot rolling, cold forming, welding (SAW, SMAW, GMAW), cutting, machining
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
EN10025-2 S235J0 Steel for SSAW Pipe Introduction
S235J0 is a non-alloy structural steel grade defined in EN 10025-2, intended for hot-rolled products and used extensively in welded structures. Delivered in the normalized rolling condition, it offers a minimum yield strength of 235 MPa for thicknesses up to 16 mm. The 'J0' designation indicates a minimum impact energy of 27 J at 0 °C (longitudinal Charpy V-notch test). This steel is particularly suited for spiral submerged arc welded (SSAW) pipes due to its good weldability, formability, and moderate strength. Typical applications include water and oil transmission pipelines, foundation piles, and structural supports. It provides a reliable balance between cost and performance for large-diameter pipe manufacturing.
EN10025-2 S235J0 Steel for SSAW Pipe Chemical Composition
The chemical composition complies with EN 10025-2:2019 for the S235J0 grade. Values are based on ladle analysis for thicknesses ≤ 40 mm. All elements are reported unless otherwise noted. For thicker sections (> 40 mm) or product forms, slightly adjusted limits may apply per the standard.
| Element | Standard Value (≤ 40 mm) | Remarks |
|---|---|---|
| Carbon (C) | ≤ 0.17 | For thickness > 40 mm, C ≤ 0.20 |
| Silicon (Si) | ≤ 0.55 (typically) | Si is not a mandatory element but may be added for deoxidation; the standard allows up to 0.55 as guidance, not specified limit for non-alloy grades |
| Manganese (Mn) | ≤ 1.40 | For thickness > 40 mm, Mn ≤ 1.50 |
| Phosphorus (P) | ≤ 0.030 | Critical for toughness |
| Sulfur (S) | ≤ 0.030 | Weldability requirement |
| Nitrogen (N) | ≤ 0.012 | For normalized steel, N may be restricted to avoid strain aging |
| Copper (Cu) | ≤ 0.55 | If copper content is higher, embrittlement precautions may be needed |
| Other elements (Cr, Ni, Mo, etc.) | Residual or incidental | Not specified but limited by the standard's general residual limits unless agreed |
EN10025-2 S235J0 Steel for SSAW Pipe Thermal and Electrical Physical Properties
Physical properties below are typical for carbon structural steels similar to S235J0 at room temperature, unless otherwise noted. These values are not mandated by EN 10025-2 but serve as engineering references. Variations may occur depending on exact composition and processing.
| Property | Typical Value | Unit | Test Condition / Remarks |
|---|---|---|---|
| Density (ρ) | 7.85 | g/cm³ | Room temperature |
| Modulus of elasticity (E) | 210 | GPa | Room temperature |
| Shear modulus (G) | 81 | GPa | Calculated from E and Poisson's ratio |
| Poisson's ratio (ν) | 0.3 | – | Within elastic range |
| Thermal expansion coefficient (α) | 12.0 | 10⁻⁶/K | 20–100 °C (average) |
| Thermal expansion coefficient (α) | 12.5 | 10⁻⁶/K | 20–200 °C |
| Thermal expansion coefficient (α) | 13.0 | 10⁻⁶/K | 20–300 °C |
| Thermal conductivity (λ) | 53 | W/(m·K) | At 20 °C |
| Thermal conductivity (λ) | 50 | W/(m·K) | At 100 °C |
| Specific heat capacity | 460 | J/(kg·K) | 20–100 °C range |
| Electrical resistivity (ρₑ) | 0.16 | Ω·mm²/m | At 20 °C |
EN10025-2 S235J0 Steel for SSAW Pipe Mechanical Properties
The following mechanical properties are in accordance with EN 10025-2 for S235J0 grade, based on normalized rolling (+N) condition. Tensile test transverse to rolling direction for flat products. Impact test longitudinal. Values depend on thickness, with multiple rows for different thickness ranges as per the standard.
| Property | Required Value | Unit | Test Condition / Thickness |
|---|---|---|---|
| Minimum Yield Strength (ReH) | 235 | MPa | t ≤ 16 mm |
| Minimum Yield Strength (ReH) | 225 | MPa | 16 mm < t ≤ 40 mm |
| Minimum Yield Strength (ReH) | 215 | MPa | 40 mm < t ≤ 63 mm |
| Minimum Yield Strength (ReH) | 215 | MPa | 63 mm < t ≤ 80 mm |
| Minimum Yield Strength (ReH) | 215 | MPa | 80 mm < t ≤ 100 mm |
| Minimum Yield Strength (ReH) | 195 | MPa | 100 mm < t ≤ 150 mm |
| Tensile Strength (Rm) | 360 – 510 | MPa | 3 mm ≤ t ≤ 100 mm |
| Tensile Strength (Rm) | 350 – 500 | MPa | 100 mm < t ≤ 150 mm |
| Elongation after fracture (A80) | ≥ 26 | % | L₀=80 mm, t ≤ 3 mm (thin products) |
| Elongation after fracture (A5.65) | ≥ 26 | % | L₀=5.65√S₀, 3 mm ≤ t ≤ 40 mm (for longitudinal specimens the minimum may be 1% higher) |
| Elongation after fracture (A5.65) | ≥ 25 | % | 40 mm < t ≤ 63 mm |
| Elongation after fracture (A5.65) | ≥ 24 | % | 63 mm < t ≤ 100 mm |
| Elongation after fracture (A5.65) | ≥ 22 | % | 100 mm < t ≤ 150 mm |
| Bend test (mandrel diameter) | ≤ 1 x thickness | – | For t ≤ 16 mm, bend angle 180°, mandrel diameter ≤ specimen thickness; for t > 16 mm, condition negotiable |
| Charpy V-notch impact energy (KV₂, longitudinal) | ≥ 27 | J | At 0 °C (J0); t ≤ 150 mm; average of 3 specimens, one value may be 70% of the required minimum |
EN10025-2 S235J0 Steel for SSAW Pipe Fully Equivalent Material Standards and Substitute Grades
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| Europe | EN 10025-2 | S235J0 | Original specification |
| International | ISO 630-2 | S235C | Equivalent with Charpy at 0 °C (27 J); confirmed by ISO/EN harmonization |
| Germany | DIN EN 10025-2 | S235J0 | Adopted EN standard |
| France | NF EN 10025-2 | S235J0 | Adopted EN standard |
| United Kingdom | BS EN 10025-2 | S235J0 | Supersedes BS 4360 Grade 40C |
| Italy | UNI EN 10025-2 | S235J0 | Adopted EN standard |
EN10025-2 S235J0 Steel for SSAW Pipe Application Introduction
S235J0 steel in the form of SSAW pipes is widely utilized in industries requiring moderate strength, good weldability, and cost-effectiveness. The normalized rolling condition ensures consistent grain structure, enhancing toughness and formability. It is ideal for large-diameter pipelines and structural applications. Common uses include:
- Water transmission mains and sewage pipes
- Oil and gas flowlines (low pressure) and gathering systems
- Foundation piles and bearing piles for civil engineering
- Structural columns and bracing for buildings and bridges
- Offshore jacket legs and secondary structural members
Due to its good cold-forming properties, it can be fabricated into various pipe fittings and custom components.
Product Applications: Spiral submerged arc welded (SSAW) pipes, Longitudinally welded line pipes, Structural hollow sections (circular, square, rectangular), Hot-rolled plates and coils for further processing, Piling pipes with or without interlock, Open sections (beams, channels) through fabrication
Processed into products: Pipe bends and elbows (hot induction or cold formed), Tees, reducers, and caps for pipeline networks, Flanges (welding neck, slip-on) machined from plate, Stiffening rings and collars for offshore jackets, Pipe shoes and supports, Diaphragm walls and caisson segments, Bollards and mooring piles
Application industries: Water and wastewater management, Oil and gas (onshore gathering & transport), Civil construction (piling and foundations), Bridge engineering, Marine and offshore structures, Mechanical and industrial fabrication
EN10025-2 S235J0 Steel for SSAW Pipe Similar / Approximate Substitute Materials
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| Europe | EN 10025-2 | S235JR | Similar strength, but impact test at +20 °C (27 J); lower toughness |
| Europe | EN 10025-2 | S235J2 | Higher toughness with impact at -20 °C (27 J); may be used when colder service required |
| Europe | EN 10025-2 | S275J0 | Higher yield strength (275 MPa) with same 0 °C impact; often used for more demanding structures |
| USA | ASTM A36/A36M | A36 | Yield 250 MPa, tensile 400-550 MPa; no Charpy requirement unless supplementary; common structural steel |
| Japan | JIS G3106 | SM400B | Yield 245 MPa, tensile 400-510 MPa; Charpy at 0 °C (27 J); used for welded structures |
| China | GB/T 700 | Q235C | Yield 235 MPa, Charpy at 0 °C (27 J); approximate equivalent in composition and properties |
| International | ISO 630-2 | S235B | Yield 235 MPa, but impact only at +20 °C; less tough variant |
Notes:
SSAW pipe production: S235J0 coils are formed into a spiral shape and welded by submerged arc process. The seam may be subject to additional non-destructive testing (UT, RT). For pressure applications, hydrostatic testing is mandatory. Weldability: Steel S235J0 has a low carbon equivalent (CEV ≤ 0.35 typically), eliminating preheating for thicknesses up to 50 mm under normal conditions. Corrosion protection: External coating (3LPE, FBE) or internal lining is recommended for buried or submerged service. Ordering notes: Specify EN 10025-2 S235J0 with required dimensions, quantity, and supplementary testing if needed (e.g., through-thickness properties, ultrasonic testing).
- Share



