
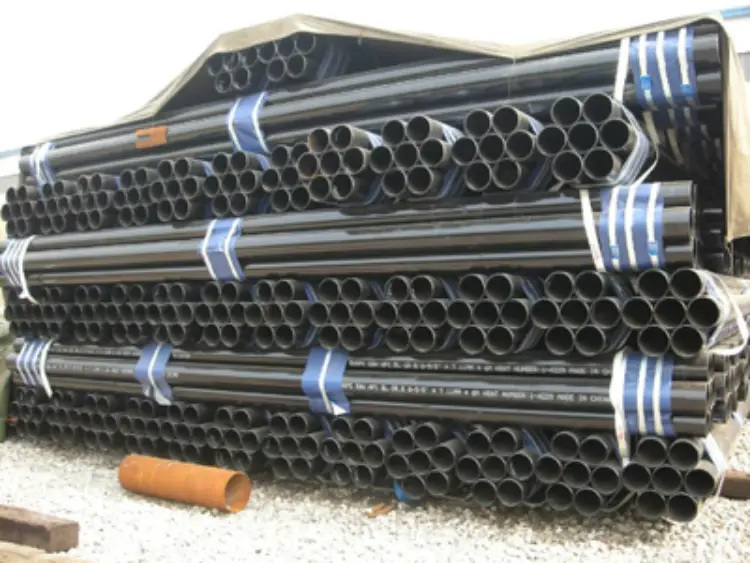
EN 10025-2 S420J0 SSAW Pipe
EN10025-2 S420J0 Structural Steel for SSAW Pipe: Properties, Equivalents & Applications
Detailed material data for S420J0 carbon structural steel according to EN 10025-2, widely used in spiral submerged arc welded (SSAW) pipes for general structural and pressure applications.
Suitable for hot rolling, cold forming, gas cutting, welding (all common methods), and machining.
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
EN 10025-2 S420J0 SSAW Pipe Introduction
S420J0 is a hot-rolled, weldable fine-grain structural steel grade defined in EN 10025-2:2019. It offers a minimum yield strength of 420 MPa for thicknesses up to 16 mm and guaranteed impact energy of 27 J at 0°C (J0 quality). The grade provides a good balance of strength, toughness, and formability, making it suitable for heavy structural components, including spiral welded (SSAW) pipes used in civil engineering, piling, and onshore/offshore structures. Its chemical composition is controlled to ensure reliable welding without significant pre-heating in moderate thicknesses. Typical delivery conditions are AR (as-rolled) or N (normalized), with options for thermomechanical rolling upon agreement.
EN 10025-2 S420J0 SSAW Pipe Chemical Composition
The chemical composition of S420J0 is controlled to ensure good weldability and mechanical properties, as specified in EN 10025-2:2019, Table 3. Maxima apply unless a range is given. The carbon equivalent value (CEV) is limited to 0.45% for thicknesses ≤ 40 mm. Optional addition of Nb, V, Ti is allowed and can influence grain refinement.
| Chemical Element | Nominal Value (wt%) | Remarks |
|---|---|---|
| Carbon (C) | ≤ 0.22 | Maximum for t ≤ 40 mm; lower C improves weldability |
| Silicon (Si) | ≤ 0.60 | - |
| Manganese (Mn) | ≤ 1.70 | - |
| Phosphorus (P) | ≤ 0.030 | - |
| Sulfur (S) | ≤ 0.030 | - |
| Nitrogen (N) | ≤ 0.014 | For long products; ≤ 0.015 for flat products |
| Copper (Cu) | ≤ 0.60 | If Cu exceeds 0.40, hot shortness may occur |
| Aluminium (Altotal) | ≥ 0.015 | Minimum when aluminium is used for deoxidation |
| Niobium (Nb) | ≤ 0.07 | Grain-refining elements: V+Nb+Ti ≤ 0.22% |
| Vanadium (V) | ≤ 0.22 | See combined limit |
| Titanium (Ti) | ≤ 0.07 | See combined limit |
| CEV (Carbon Equivalent) | ≤ 0.45 | CEV = C + Mn/6 + (Cr+Mo+V)/5 + (Ni+Cu)/15; for t ≤ 40 mm |
EN 10025-2 S420J0 SSAW Pipe Thermal and Electrical Physical Properties
Typical physical properties of non-alloy structural steel relevant for design and processing. These values are representative for carbon-manganese steels at room temperature unless otherwise stated; slight variations may occur depending on exact composition and processing history. The data are useful for heat transfer calculations and welding pre-heat determination.
| Physical Property | Typical Value | Unit | Test Condition / Remarks |
|---|---|---|---|
| Density (ρ) | 7.85 | g/cm³ | At 20°C |
| Elastic modulus (E) | 210 | GPa | At 20°C |
| Shear modulus (G) | 81 | GPa | At 20°C; calculated from E and ν |
| Poisson's ratio (ν) | 0.3 | - | At 20°C |
| Thermal expansion coefficient (α) | 12.0 | 10−⁰/K | For the range 20–100°C |
| Thermal expansion coefficient (α) | 12.5 | 10−⁰/K | For the range 20–200°C |
| Thermal expansion coefficient (α) | 13.5 | 10−⁰/K | For the range 20–400°C |
| Thermal conductivity (λ) | 53 | W/(m·K) | At 20°C |
| Thermal conductivity (λ) | 50 | W/(m·K) | At 100°C |
| Thermal conductivity (λ) | 45 | W/(m·K) | At 300°C |
| Specific heat capacity (cp) | 460 | J/(kg·K) | At 20°C |
| Specific heat capacity (cp) | 520 | J/(kg·K) | At 500°C |
| Electrical resistivity (ρe) | 0.20 – 0.25 | Ω·mm²/m | At 20°C; typical range |
EN 10025-2 S420J0 SSAW Pipe Mechanical Properties
Mechanical property requirements for S420J0 in the delivery condition according to EN 10025-2:2019, Table 5. Yield and tensile properties vary with product thickness. Impact testing is mandatory at 0°C (longitudinal specimens). The bending test is performed with a mandrel diameter depending on thickness and test direction.
| Property | Required Value | Unit | Test Condition / Thickness (mm) |
|---|---|---|---|
| Yield strength (ReH) | 420 | MPa | t ≤ 16 |
| Yield strength (ReH) | 400 | MPa | 16 < t ≤ 40 |
| Yield strength (ReH) | 390 | MPa | 40 < t ≤ 63 |
| Yield strength (ReH) | 370 | MPa | 63 < t ≤ 80 |
| Yield strength (ReH) | 360 | MPa | 80 < t ≤ 100 |
| Yield strength (ReH) | Consult manufacturer | MPa | 100 < t ≤ 150 |
| Tensile strength (Rm) | 520 – 680 | MPa | t ≤ 40 |
| Tensile strength (Rm) | 510 – 680 | MPa | 40 < t ≤ 80 |
| Tensile strength (Rm) | 500 – 670 | MPa | 80 < t ≤ 100 |
| Tensile strength (Rm) | Consult manufacturer | MPa | 100 < t ≤ 150 |
| Elongation (A) | ≥ 19 | % | Longitudinal; t ≤ 40 |
| Elongation (A) | ≥ 18 | % | Longitudinal; 40 < t ≤ 63 |
| Elongation (A) | ≥ 17 | % | Longitudinal; 63 < t ≤ 100 |
| Elongation (A) | Consult manufacturer | % | Longitudinal; t > 100 |
| Impact energy (KV) | ≥ 27 | J | Longitudinal; at 0°C; 10x10 mm specimen where possible |
| Bend test (mandrel diameter) | 2t | - | Longitudinal; for t ≤ 16; 180° bend |
| Bend test (mandrel diameter) | 3t | - | Longitudinal; for 16 < t ≤ 25 |
| Bend test (mandrel diameter) | 4t | - | Longitudinal; for 25 < t ≤ 40 |
EN 10025-2 S420J0 SSAW Pipe Fully Equivalent Material Standards and Substitutable Grades
| Country / Region | Standard | Grade | Remarks |
|---|---|---|---|
| International (ISO) | ISO 630-2:2011 | S420J0 | Identical in concept; same chemical and mechanical requirements; J0 = 0°C impact. |
| European Union | EN 10025-2:2019 | S420J0 | The original grade defined in this standard. |
| Germany | DIN EN 10025-2:2019 | S420J0 | Adopted European standard; identical requirements. |
| United Kingdom | BS EN 10025-2:2019 | S420J0 | British adoption; fully equivalent. |
| China | GB/T 1591-2018 | Q420C | Mechanical properties comparable (420 MPa min, 0°C impact) but with some differences in chemical composition limits. Verify CEV and trace elements. |
EN 10025-2 S420J0 SSAW Pipe Application Introduction
S420J0 steel is predominantly used in welded structural applications where a combination of strength, notch toughness at low temperatures, and good weldability is required. In the form of SSAW (spiral submerged arc welded) pipes, it serves as a cost-effective solution for large-diameter pipelines and tubular structures. Typical fields of use:
Product Applications: SSAW (spiral welded) steel pipes for water mains and penstocks, Longitudinally welded pipes and hollow sections, Heavy H-beams, I-beams and columns, Sheet piling sections, Structural plates for bridges and buildings, Wind tower segments, Hydrostatic penstocks and spiral casings
Processed into products: Pipe spools and fittings for SSAW pipelines, Flanges, stiffeners, and gusset plates, Anchor piles and bearing piles, Bridge bearings and expansion joints, Support legs and bracing for offshore platforms, Welded joint plates in heavy machinery frames, Tubular transition pieces in tower constructions
Application industries: Civil and structural engineering, Water and waste-water transmission, Oil & gas (onshore gathering lines, low-pressure conduits), Offshore structural (secondary members and piling), Bridge construction, Wind turbine tower structures, Shipbuilding (non-critical structural components)
EN 10025-2 S420J0 SSAW Pipe Similar or Substitute Material Recommendations
| Country / Region | Standard | Grade | Remarks |
|---|---|---|---|
| USA | ASTM A572/A572M | Grade 60 (Type 1 or 2) | Min. yield 415 MPa, tensile 520 MPa. No mandatory impact test; supplementary test for 0°C can be agreed. Chemistry differs (higher Mn). Not a direct J0 equivalent. |
| Japan | JIS G3106:2015 | SM490B | Min. yield 325 MPa (for t ≤ 16), tensile 490-610 MPa. Impact 0°C ≥27J. Strength is lower than S420; suitable where lower strength is acceptable. |
| Japan | JIS G3106:2015 | SM520B | Min. yield 365 MPa, tensile 520-640 MPa. Impact 0°C ≥27J. Higher strength than SM490B but still below S420. |
| China | GB/T 1591-2018 | Q355C | Min. yield 355 MPa, tensile 470-630 MPa, 0°C impact. Lower strength level; an alternative only if design allows. |
| Russia/ CIS | GOST 27772-88 | C440 (S440) | Min. yield 440 MPa for shapes. 0°C impact option available. Chemical composition not fully aligned; requires case-by-case evaluation. |
Notes:
Welding considerations: S420J0 exhibits good weldability with all common processes (SMAW, SAW, GMAW). For thicknesses above 30 mm, a moderate preheat (about 75-125°C) is recommended to avoid cold cracking. Post-weld heat treatment (PWHT) is normally not required for SSAW pipe produced from this grade, but a stress-relief treatment may be applied to cold-formed spirals to meet dimensional tolerance and residual stress requirements. Inspection: Ultrasonic testing of the weld seam and hydrostatic testing are standard for SSAW pipes destined for pressure applications. Certification: EN 10204 type 3.1 inspection certificate is typically provided.
- Share



