
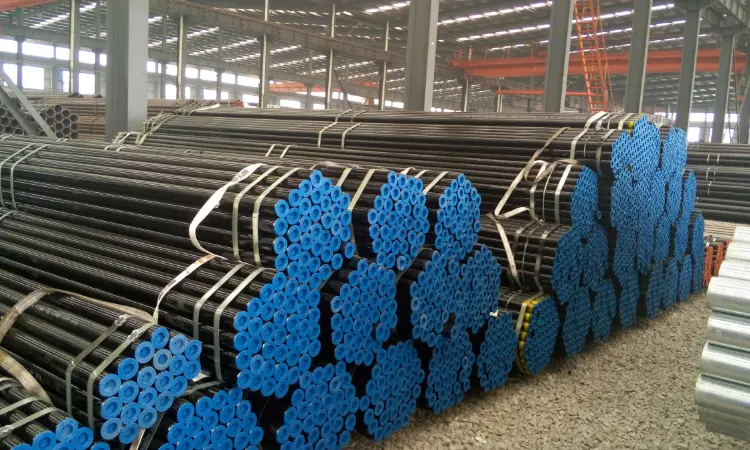
JIS G3106 SM490B Steel for SSAW Pipe
JIS G3106 SM490B Structural Steel for SSAW Pipe – Properties & Equivalents
Detailed material data for SM490B steel according to JIS G3106, widely used in spiral submerged arc welded (SSAW) pipes. Includes chemical composition, mechanical and physical properties, international equivalents, and application guidance.
Hot rolling, thermo-mechanical rolling, normalizing, welding (SAW, SSAW), cold forming, cutting, machining
- Phone : +8618037372205
- Email : [email protected]
- WhatsApp: Contact via Whtsapp
- WeChat: +8618037372205
JIS G3106 SM490B Steel for SSAW Pipe Introduction
JIS G3106 SM490B is a hot-rolled weldable structural steel with a minimum yield strength of 325 MPa (for thickness ≤16 mm). It offers a good balance of strength, ductility, and weldability, making it a preferred choice for structural components and tubular products. As a killed steel with fine grain practice, SM490B exhibits reliable low-temperature toughness (27 J min at 0°C). The grade is frequently supplied as plates, coils, and strips, and is subsequently formed into SSAW (spiral submerged arc welded) pipes for water transmission, piling, and structural applications. Its controlled carbon equivalent ensures ease of welding without preheating under normal conditions, supporting cost-effective fabrication.
JIS G3106 SM490B Steel for SSAW Pipe Chemical Composition
The chemical requirements for SM490B according to JIS G3106:2015. Values are maximum unless a range is indicated. The steel is fully killed with fine grain practice. Carbon equivalent (Ceq) is usually limited to 0.44% max for thickness ≤50 mm to ensure weldability.
| Chemical Element | Standard Value (max, %) | Remarks |
|---|---|---|
| Carbon (C) | ≤ 0.18 | Ladle analysis |
| Silicon (Si) | ≤ 0.55 | |
| Manganese (Mn) | ≤ 1.60 | |
| Phosphorus (P) | ≤ 0.030 | |
| Sulfur (S) | ≤ 0.030 | |
| Carbon Equivalent (Ceq) | ≤ 0.44 (typically) | For thickness ≤50 mm, Ceq = C + Mn/6 + (Cu+Ni)/15 + (Cr+Mo+V)/5; subject to agreement |
JIS G3106 SM490B Steel for SSAW Pipe Thermal & Electrical Physical Properties
These values are typical for low‑carbon manganese structural steels similar to SM490B at room temperature, unless otherwise noted. They are not mandated by JIS G3106 but are widely accepted for engineering calculations.
| Property | Standard Requirement (typical) | Unit | Test Condition |
|---|---|---|---|
| Density (ρ) | 7.85 | g/cm³ | 20 °C |
| Modulus of elasticity (E) | 205 | GPa | 20 °C |
| Shear modulus (G) | 79 | GPa | 20 °C |
| Poisson's ratio (ν) | 0.30 | – | 20 °C |
| Thermal expansion coefficient (α) | 12.0 | ×10⁻⁶/K | 20 – 100 °C |
| Thermal expansion coefficient (α) | 13.0 | ×10⁻⁶/K | 20 – 300 °C |
| Thermal conductivity (λ) | 51 | W/(m·K) | 20 °C |
| Specific heat capacity (Cp) | 486 | J/(kg·K) | 20 °C |
| Electrical resistivity (ρ_e) | 0.20 – 0.25 | µΩ·m | 20 °C |
JIS G3106 SM490B Steel for SSAW Pipe Mechanical Properties
Tensile and impact properties as required by JIS G3106. Values depend on product thickness. The steel is supplied in as-rolled, normalized, or TMCP condition. Charpy V-notch impact test is conducted at 0°C on longitudinal specimens (full-size).
| Property | Standard Requirement | Unit | Test Condition |
|---|---|---|---|
| Yield strength (ReH) | ≥ 325 | MPa | t ≤ 16 mm |
| Yield strength (ReH) | ≥ 315 | MPa | 16 mm < t ≤ 40 mm |
| Yield strength (ReH) | ≥ 295 | MPa | 40 mm < t ≤ 75 mm |
| Yield strength (ReH) | ≥ 295 | MPa | 75 mm < t ≤ 100 mm |
| Tensile strength (Rm) | 490 – 610 | MPa | t ≤ 100 mm |
| Elongation (A) | ≥ 22 | % | t ≤ 5 mm, gauge length: JIS No. 5 specimen |
| Elongation (A) | ≥ 17 | % | 5 mm < t ≤ 16 mm, JIS No. 1A specimen |
| Elongation (A) | ≥ 21 | % | 16 mm < t ≤ 50 mm, JIS No. 1A specimen |
| Elongation (A) | ≥ 23 | % | > 40 mm, JIS No. 4 specimen (if applicable) |
| Charpy impact (KV₂) | ≥ 47 (min), ≥ 27 (min individual) | J | Longitudinal, 0°C, full-size specimen |
| Bend test | No cracks in outer surface (optional) | – | 180° bend, d=1.5a for t ≤16 mm (by agreement) |
JIS G3106 SM490B Steel for SSAW Pipe Equivalent Standards and Direct Substitute Grades
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| European Union | EN 10025-3 | S355N | Normalized structural steel, comparable strength and toughness at 0°C |
| China | GB/T 1591 | Q355D | Low-alloy high-strength structural steel, impact at -20°C → slight overmatch in toughness |
| India | IS 2062 | E350 BR | Hot-rolled structural steel with B-quality, impact at 0°C |
| Japan | JIS G3136 | SN490B | Steel for building structures, very similar chemistry and strength |
| International | ISO 630-2 | E355B | Fine-grain structural steel, impact at 0°C |
JIS G3106 SM490B Steel for SSAW Pipe Application Introduction
SM490B SSAW pipes are widely utilized where a balance of strength, weldability, and cost efficiency is required. The spiral submerged arc welding process allows the production of large-diameter pipes from hot-rolled coils of SM490B. Typical applications are described below.
Product Applications: SSAW large-diameter water pipelines (24" – 120"), Structural hollow sections and tubular columns, Bridge girders and trusses, Piling pipes and foundation casings, Penstocks and hydro power conduits
Processed into products: Pipe barrels and can assemblies, Flanges and end caps welded to SSAW pipes, Pipe shoes and support plates, Stiffener rings and connector pieces, Reducer and tee fittings made from SM490B plate
Application industries: Civil engineering and construction (buildings, bridges, stadiums), Water supply and drainage (transmission mains, penstocks), Oil and gas (low-pressure gathering lines, casing), Offshore and marine (jacket legs, piling, structural supports), Infrastructure (sign poles, lighting columns, structural hollow sections)
JIS G3106 SM490B Steel for SSAW Pipe Similar Grades for Alternative Selection
These materials offer close but not identical mechanical or chemical properties. Selection should consider specific thickness and impact test temperature.
| Country/Region | Standard | Grade | Remarks |
|---|---|---|---|
| USA | ASTM A572/A572M | Grade 50 [345] | Yield 345 MPa (≤50 mm), but impact test not mandatory unless specified as Grade 50S |
| European Union | EN 10025-2 | S355J2+N | Same strength level, impact at -20°C; widely available as plates and sections |
| Russia | GOST 27772 | C355 (С355) | Killed structural steel with similar carbon equivalent, impact test at -20°C |
| China | GB/T 700 | Q390D | Higher yield (390 MPa), but comparable weldability and toughness |
| Japan | JIS G3101 | SS490 | Similar tensile range, but less strict on impact toughness (only by agreement) |
Notes:
Welding considerations: SM490B has a controlled carbon equivalent (≤0.44), allowing welding without preheat for moderate thicknesses. Low-hydrogen welding consumables matching the strength level (e.g., E4918 per AWS A5.1 or equivalent) are recommended. Post-weld heat treatment is not normally required. For SSAW pipe production, the strip edges are precisely prepared and welded using submerged arc welding with filler wires compatible with SM490B chemistry. The final pipe may be hydrotested and coated for corrosion protection depending on service conditions.
- Share



